



Stanzstifte für Edelstahlstanzen: Material- und Beschichtungsoptionen
There is no single best material or coating for punch pins used in stainless steel stamping. The right combination depends on the stainless grade and condition, Blechdicke, Stanzgeometrie, Produktionsvolumen, Schmierung, die alignment, Freigabe, and the failure mode already appearing in production.
A punch substrate provides the bulk toughness, Druckfestigkeit, and edge support. Heat treatment establishes its usable hardness and fracture resistance. Surface finish affects friction and material pickup. The coating or surface treatment then modifies wear, Wärme, and sliding behavior. Choosing only one of these elements rarely solves the complete problem.
This guide focuses on punch pins used to pierce or blank stainless steel sheet. It does not assume that the punch itself must be made from stainless steel. Für umfassendere Informationen zu Stempeltypen, system-level material selection, Freigabe, Toleranzen, und Beschaffung, Siehe die Leitfaden für Stanzenwerkzeuge (Schlussfolgerung).
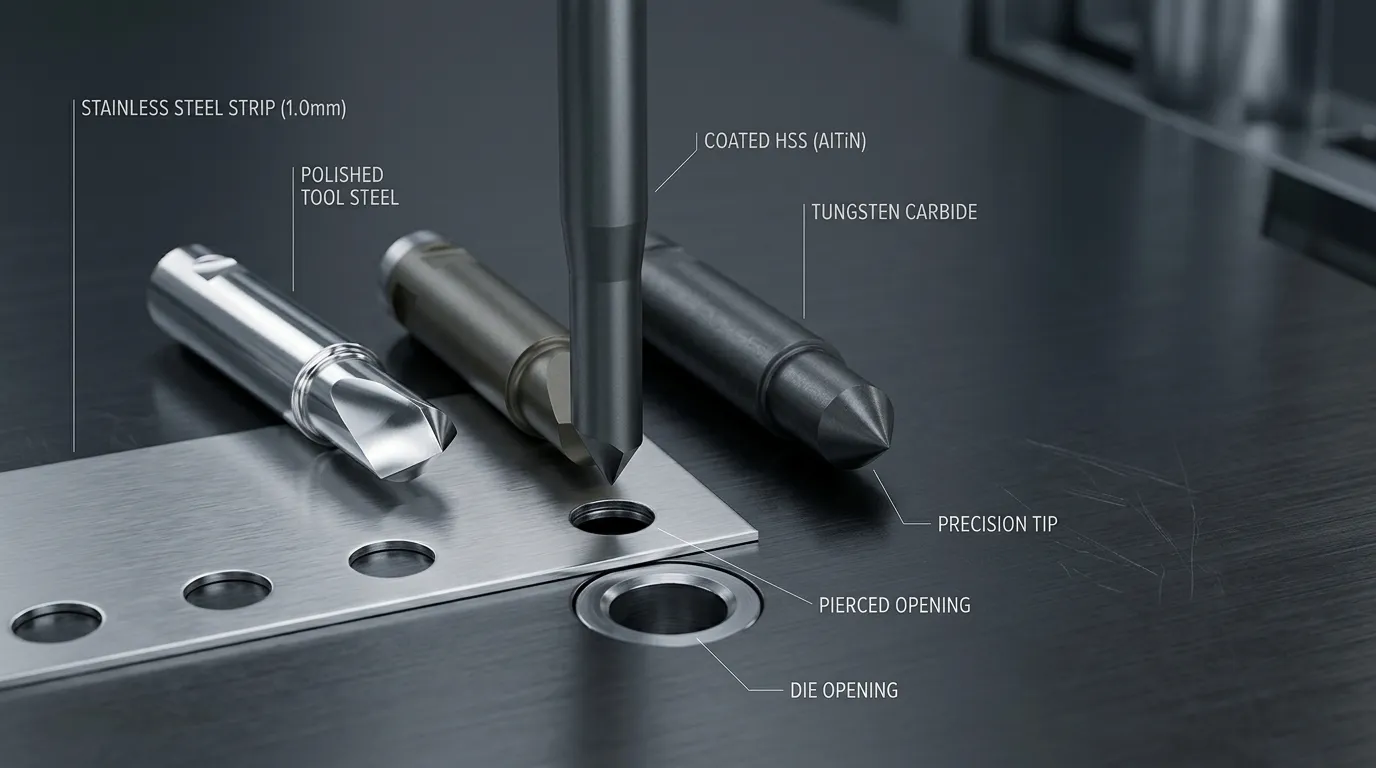
Warum Edelstahl die Auswahl von Stanzstiften ändert
Stainless steel is not one uniform work material. Austenitic, ferritic, martensitic, and duplex grades have different mechanical properties and forming behavior. Das WorldStainless Übersicht der Edelstahlfamilien is useful background, but the tooling decision must go further than identifying the family name.
The supplier or tool engineer should know:
- the exact stainless grade;
- Blechdicke;
- temper, Härte, or tensile condition;
- Oberflächenzustand;
- pierced-hole or blank geometry;
- expected production quantity;
- lubrication method or restrictions;
- current punch material and coating;
- the actual failure seen in production.
Stainless applications often create high contact pressure, Gleitreibung, and heat at the punch surface. Under unfavorable conditions, workpiece material can transfer onto the punch. This adhesive wear process is commonly described as galling or material pickup.
Eine peer-reviewte Begutachtung von Galling beim Metallformen explains that friction, Oberflächenzustand, Druck, Temperatur, and wear development interact during the process. Once pickup begins, the roughened punch surface can attract more material, increase stripping force, damage the sheet surface, and accelerate further wear.
Stainless sheet may also work-harden near the cutting zone. Thicker or stronger material raises the load on the cutting edge. These conditions make it risky to choose a punch only by nominal hardness.
Wählen Sie das Lochsubstrat aus, bevor Sie die Beschichtung auswählen
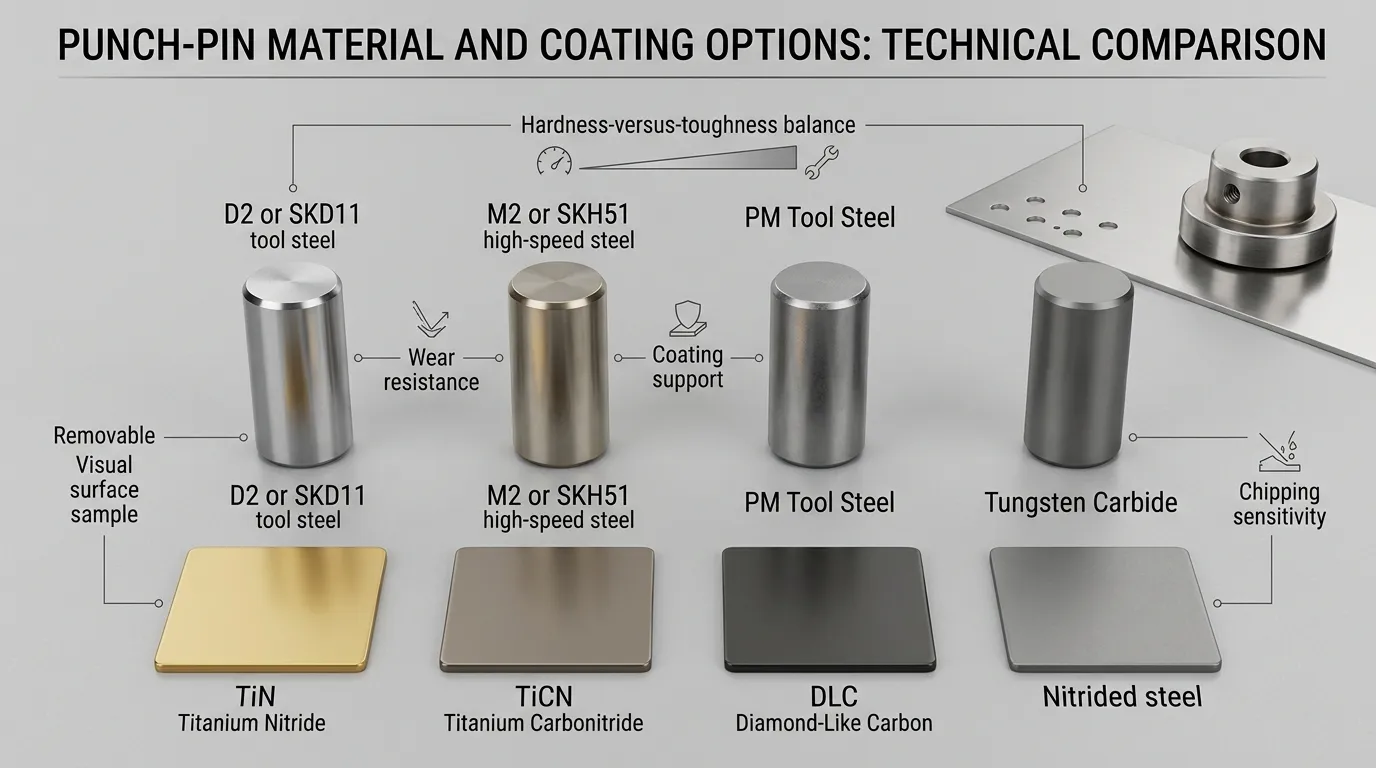
The coating is supported by the material underneath it. A hard coating on an unsuitable, poorly heat-treated, or damaged substrate can still crack, delaminate, Chip, or fail with the cutting edge.
The main punch-material options should be compared using several properties:
| Stanzsubstrat | Hauptstärken | Hauptbeschränkungen | Typischer Grund, es in Betracht zu ziehen |
|---|---|---|---|
| D2- oder SKD11-Typ Werkzeugstahl | Verschleißfestigkeit, Druckfestigkeit, Dimensionsstabilität | Can be less tolerant of impact, Ablenkung, or sharp stress concentrations than tougher grades | Stabile Geometrie und moderate verschleißbedingte Produktion |
| M2, SKH51, or SKH9 HSS | Better balance of wear resistance, Zähigkeit, und Hitzebeständigkeit | Higher cost than conventional tool steel; still dependent on correct heat treatment | Stainless, thicker sheet, coated punches, or higher production demands |
| PM-Werkzeugstahl | Starkes Gleichgewicht zwischen Verschleiß und Zähigkeit und gleichmäßigere Mikrostruktur | Premiummaterialkosten und qualitätsspezifische Verarbeitungsanforderungen | Wenn herkömmlicher Stahl zu schnell abnutzt, aber Hartmetall zu spröde ist |
| Stoßfester Werkzeugstahl | Hohe Zähigkeit und Widerstandsfähigkeit gegen schlagbedingte Brüche | Geringere Verschleißfestigkeit als stark legierte Verschleißgrade | Abplatzen oder Aufprall sind wichtiger als allmählicher Verschleiß |
| Wolframkarbid | Very high hardness, Druckfestigkeit, und Verschleißfestigkeit | Brittle under misalignment, Schock, Ablenkung, or poor edge support | Stabile, verschleißige Produktion mit starren Werkzeugen |
| Edelstahl wie SUS420 oder SUS440 | Korrosionsbeständigkeit und Polierbarkeit | Nicht automatisch das beste Substrat zum Piercen von Edelstahlplatten | korrosive Umgebungen oder Anwendungen, in denen der Stempel selbst korrosionsbeständig sein muss |
D2 or SKD11 for Stable, Wear-Led Applications
D2-class cold-work tool steel is widely used where wear resistance and compressive strength are important. Material documentation for BÖHLER K110, a D2-class steel, lists stamping and blanking among its applications and emphasizes wear resistance and dimensional stability.
D2 or SKD11 may be a reasonable starting point when:
- the punch has a robust cross-section;
- alignment and clearance are controlled;
- production volume is moderate;
- gradual wear is the main concern;
- sudden chipping or bending is not occurring.
It becomes a weaker choice when the punch is very slender, has sharp corners, experiences side loading, or breaks before the cutting edge wears out. In diesen Fällen, additional hardness may make the problem worse rather than better.
M2, SKH51, or SKH9 When Toughness and Heat Resistance Matter More
High-speed steel is commonly evaluated when the punch needs a stronger balance of wear resistance, Zähigkeit, and resistance to heat generated during repeated cycling.
Technische Anleitung von CONIC auf Werkzeugmaterialien associates M2-type material with stainless steel, thicker sheet, coating use, and larger production quantities. That does not make M2 a universal answer, but it explains why HSS often appears in stainless stamping recommendations.
SunshinePros Hochgeschwindigkeits-Stahlstanz page lists SKH51 and SKH9 among its material options, along with vacuum heat treatment, Präzisionsschleifen, EDM, and optional TiN or TiCN coatings. These are company-specific product options, not fixed specifications for every application.
HSS is worth evaluating when:
- D2 wears or chips too quickly;
- surface heat is significant;
- the punch will receive a PVD coating;
- production volume justifies a higher-cost substrate;
- the geometry needs more fracture resistance than conventional wear steel provides.
PM-Werkzeugstahl für ein höheres Verhältnis zwischen Verschleiß und Zähigkeit
Powder-metallurgy tool steels are useful when both wear and fracture resistance matter. Their more uniform microstructure can provide a better combination of properties than many conventionally produced tool steels.
Zum Beispiel, the manufacturer describes BÖHLER K490 MICROCLEAN as a PM cold-work steel combining wear resistance, Druckfestigkeit, Zähigkeit, and dimensional stability for applications that include stamping and blanking.
PM steel may be justified when:
- conventional D2-type steel wears too quickly;
- HSS does not provide the required service interval;
- carbide chips under the existing geometry or loading;
- downtime costs more than the material upgrade;
- repeated regrinding and stable dimensional behavior are important.
The recommendation must still be grade-specific. “PM steel” is a manufacturing category, not one standardized set of properties.
Carbide for Stable High-Wear Conditions, Not Every High-Volume Job
Tungsten carbide offers high hardness, Druckfestigkeit, and resistance to abrasive wear. It can be effective in stable, high-volume applications where the punch receives rigid support and loading remains predictable.
Its main limitation is brittleness. Carbide is less forgiving of:
- Fehlstellung;
- Schlagabwehr;
- impact or interrupted loading;
- weak corner geometry;
- unzureichende Unterstützung;
- slug interference;
- Seitenbelastung;
- Falsche Freigabe.
A carbide punch that chips after a few cycles is not improved by selecting an even harder carbide grade without correcting the mechanical cause.
SunshinePros Hartmetallstanz page lists tungsten carbide, Präzisionsschleifen, EDM, customized dimensions, and TiN, TiCN, or DLC coating options. Suitability still requires a review of the punch geometry, Werkstück, Pressebedingungen, und Ausfallgeschichte.
Wenn ein Edelstahl-Stanz tatsächlich die Voraussetzung ist
A punch used on stainless steel does not automatically need a stainless substrate.
Corrosion-resistant grades such as SUS420 or SUS440 may be selected when the tool itself is exposed to moisture, corrosive substances, frequent cleaning, or an environment where rust resistance matters. SunshinePro lists these grades on its separate stainless punch-pin product page.
That is a different engineering requirement from selecting a wear-resistant punch for stainless sheet. In many stamping applications, HSS, PM steel, conventional tool steel, or carbide may provide a more useful balance of wear, Zähigkeit, and edge stability.
Passen Sie die Beschichtung oder Oberflächenbehandlung an den Versagensmodus an
Coating choice should begin with the observed surface failure.
- Klebstoffverschleiß oder Galling: prioritize low friction, resistance to material transfer, Oberflächenvorbereitung, und Schmierung.
- Abrasiver Verschleiß: prioritize surface hardness and resistance to gradual material loss.
- High heat: review thermal stability and compatibility with the substrate’s heat-treatment condition.
- Chipping or fracture: correct the substrate, Geometrie, Ausrichtung, or loading before focusing on the coating.
- Hohe Strippkraft: inspect pickup, Finish, Schmierung, and punch withdrawal conditions.
A coating name alone is not enough. Performance also depends on coating thickness, Adhäsion, Absetzungsprozess, edge preparation, Substrathärte, Betriebstemperatur, und Oberflächenbehandlung.
TiN and TiCN Are Common Options, Not Universal Answers
TiN is one of the most familiar hard coatings used on tooling. It can improve wear resistance in suitable systems, but it should not automatically be described as the preferred stainless-steel coating.
Zum Beispiel, Dayton Laminas Beschichtungsführung assigns different treatments to adhesive wear, Abrasiver Verschleiß, Wärme, and specific work materials. Its recommendations also show that TiN is not universally preferred for stainless applications.
TiCN is commonly considered where higher wear resistance and improved sliding behavior are required. It may be evaluated for abrasive wear or material-pickup problems, but its performance still depends on substrate support, Oberflächenvorbereitung, coating quality, und Betriebsbedingungen.
SunshinePro lists TiN and TiCN as available options on its HSS and stainless-steel punch-pin pages. The final selection should be based on the actual application rather than coating popularity.
AlTiN oder AlCrN für hitzebedingte Bedingungen
AlTiN and AlCrN coatings are often considered where elevated surface temperature and demanding wear conditions are central concerns.
Before selecting either coating, Bestätigen:
- the substrate’s tempering resistance;
- coating-process temperature;
- required friction behavior;
- edge preparation;
- Beschichtungsadhäsion;
- whether heat or galling is the dominant failure.
A heat-resistant coating will not correct an unsupported edge or a punch that bends under load.
DLC und schmierende Mehrschichtsysteme für Klebstoffverschleiß
DLC and other low-friction multilayer systems may be considered where adhesive wear, Ärger, and high stripping force dominate.
Technische Beratung von Werkzeugherstellern wie Partnerpräzision connects low-friction coating selection with lubrication restrictions, punch dimensions, Blechdicke, and deflection. This is important because a lubricious surface can reduce friction, but it cannot stabilize a weak punch geometry.
DLC suitability depends on the substrate, Absetzungsprozess, service temperature, Beschichtungsadhäsion, and edge loading. SunshinePro lists DLC on its carbide-punch page, but that does not confirm availability or suitability for every punch material.
Nitritern, wenn eine Diffusionsbehandlung zum Behandlungsplan passt
Nitriding hardens the punch surface by diffusion rather than adding a separate deposited layer. It can be useful where surface hardness and geometry coverage are important.
Its selection should consider:
- substrate compatibility;
- case depth;
- Erforderliche Oberflächenbehandlung;
- Dimensionsänderung;
- Nachschleifzuschuss;
- whether the treated layer will remain after sharpening.
Nitriding should not be described as a SunshinePro capability unless confirmed for the specific order. It remains a general technical option to discuss with the tooling and treatment supplier.
Diagnostizieren Sie den Fehler, bevor Sie das Werkzeug aufrüsten
A more expensive material or coating is useful only when it addresses the actual failure.
| Beobachtete Symptome | Wahrscheinlicher Mechanismus | Überprüfen Sie vor dem Upgrade | Mögliche Materialrichtung | Mögliche Oberflächenrichtung |
| Edelstahlablagerungen auf der Stanze | Galling oder Klebstoffverschleiß | Ziel, Schmierung, Wärme, Freigabe, stripping action | Behalten Sie ein robustes Substrat, wenn es nicht verformt oder absplittert | Low-friction PVD, DLC-type system, Nitriterung, or improved polishing depending on conditions |
| Allmähliche Kantenabrundung | Abrasiver Verschleiß | Workpiece condition, Freigabe, punch hardness, Produktionsvolumen | HSS, PM steel, or carbide if the process is stable | TiCN oder eine andere verschleißfokussierte Beschichtung |
| Kleine Splitter an der Schneide | Lokaler Bruch oder unzureichende Zähigkeit | Edge geometry, Ausrichtung, Ecken, Stempelstütze, Wärmebehandlung | Tougher HSS, PM steel, or shock-resistant steel | Behandle die Beschichtung nicht als Hauptlösung |
| Plötzlicher Stempelbruch | Mechanical overload, Ablenkung, Fehlstellung, or brittle substrate | Anleitung, Gefolgsgeld, Freigabe, slug interference, punch length | Zähigkeitsgeführtes Substrat nach Korrektur der mechanischen Ursache | Die Beschichtung ist sekundär |
| Kantenverformung oder Rollover | Inadequate hardness, Druckfestigkeit, oder Unterstützung | Wärmebehandlung, punch load, Dicke, Geometrie | Higher-strength tool steel, HSS, PM steel, or carbide where stable | Verschleißbeschichtung nur nach der Substratkorrektur |
| Hohe Rückzugskraft | Pickup, poor stripping, Raues Finish, or inadequate lubrication | Stripper condition, punch surface, Schmiermittel, Seitenbelastung | Halte ausreichend Zähigkeit für die Entzugslast | Reibungsarme Behandlung, wo kompatibel |
Die allgemeine Frakturdiagnose gehört in den separaten Leitfaden zu Stanzbruch in Stempelwerkzeugen. The critical point here is that chipping and breakage often indicate a bulk-material or mechanical problem, not a missing coating.
Überprüfe die Geometrie und die Bedingungen der Stantrize, bevor du das Material beschuldigst
The punch operates as part of a complete die system. Before changing the substrate or coating, inspect the conditions that control how the load reaches the cutting edge.
- Confirm punch alignment. Misalignment creates uneven edge loading and can chip even a premium punch.
- Review punch-and-die clearance. Clearance should match the workpiece material and thickness. An unsuitable value can increase force, Burr-Formation, Verschleiß, and fracture risk.
- Inspect the stripper and guide system. Poor guidance or abnormal stripping can bend the punch during withdrawal.
- Check the retainer and mounting condition. Movement at the head or shank changes how the punch is loaded.
- Inspect for slug interference. A trapped or pulled slug can create sudden overload.
- Review the punch surface. Grinding marks, Schäden, or pickup can accelerate galling.
- Confirm lubrication. Restricted lubrication changes the friction and coating requirements.
- Account for coating thickness. Final dimensions and tolerances should reflect the complete coated condition.
Das Leitfaden für die Stanzenkomponenten provides broader information about punches, Pins, Buchsen, Leitkomponenten, and wear parts.
Kleine und schlanke Schläge brauchen eine Härte-zu-erste Bewertung
A small-diameter or high-aspect-ratio punch can deflect before the cutting edge reaches its nominal material limit.
Risk rises when the punch has:
- Übermäßige ununterstützte Länge;
- Scharfe Ecken;
- Enge Abschnitte;
- Seitenbelastung;
- interrupted contact;
- poor guidance;
- heavy stripping force.
In this situation, selecting carbide or maximizing hardness can increase chipping risk. A tougher HSS or PM steel, kürzere, nicht gestützte Länge, stronger guidance, and improved corner design may provide a better result than a harder coating.
Nutzen Sie Anwendungsbedingungen, um das Material-Beschichtungssystem zu englisten
The following matrix provides a starting direction, not a final engineering specification.
| Anwendungszustand | Substratrichtung zu bewerten | Oberflächenrichtung zur Bewertung | Überprüfen Sie zuerst |
| Moderate volume, robust geometry, controlled process | D2/SKD11 oder HSS | Polished uncoated surface, TiN, TiCN, or nitriding depending on wear | Grade, Dicke, Freigabe, Schmierung |
| Hochvolumen-Abrasivverschleiß | HSS, PM steel, oder Karbid | Verschleißfokussierte PVD-Behandlung | Trasse, edge support, regrinding plan |
| Galling mit sichtbarer Materialaufnahme | Robuster HSS- oder PM-Stahl, wenn das Substrat stabil bleibt | Low-friction PVD, DLC-type system, multilayer coating, or nitriding | Ziel, Schmiermittel, Wärme, stripper action |
| Kleiner oder schlanker Punch mit Absplittern | Tough HSS, PM steel, or shock-resistant steel | Die Beschichtung wird erst nach der Bruchursache kontrolliert | Nicht unterstützte Länge, Anleitung, Ecken, Ausrichtung |
| Dickes oder hochbelastendes Edelstahlblech | HSS or PM steel; carbide only in a rigid, stable setup | Hitze- and wear-appropriate coating | Punch load, Freigabe, Unterstützung, Pressezustand |
| Umgebung für korrosives Werkzeug | Korrosionsbeständiger Werkzeugstahl, wo die Last es erlaubt | Behandlung, die mit dem gewählten Edelstahlsubstrat kompatibel ist | Ob Korrosionsbeständigkeit oder Stempelleistung oberste Priorität hat |
Do not use this matrix to skip testing or drawing review. Two applications using the same stainless grade may need different punches because the thickness, hole diameter, punch length, Schmierung, Druckgeschwindigkeit, and service expectations are different.
Vergleichen Sie Werkzeugoptionen nach Wartbarkeit und Kosten pro Treffer
Initial purchase price is a weak basis for comparing punch options.
A more useful evaluation includes:
- hits between sharpening or replacement;
- unplanned downtime;
- tool-change frequency;
- regrinding cost;
- recoating feasibility;
- dimensional loss after sharpening;
- scrap and surface-damage risk;
- inspection time;
- Ersetzungslieferzeit;
- probability of sudden fracture.
A PM steel or carbide punch may cost more at the start but reduce cost per hit in a stable application. The same upgrade can become expensive if the punch continues to break because of misalignment or poor guidance.
Regrinding also changes the tool. It can reduce punch length, remove the treated surface near the cutting edge, alter corner geometry, and affect shut height or penetration. Recoating is possible only when enough usable material remains and the surface can be restored to the condition required by the coating supplier.
The service plan should therefore be considered before the original material and coating are selected.
Informationen, die in eine individuelle Lochstift-RFQ aufgenommen werden sollten
A supplier cannot make a defensible recommendation from the phrase “punch for stainless steel” alone.
Include the following information in the request:
- stainless grade and family;
- Blechdicke;
- temper, Härte, or tensile condition;
- part and hole drawing;
- Stanzdurchmesser, Länge, Kopf, Shank, and corner geometry;
- required dimensional tolerances;
- die clearance where known;
- press type and stroke rate;
- Erwartetes Produktionsvolumen;
- target service interval;
- lubricant or dry-running restriction;
- current punch material and hardness;
- current coating or treatment;
- photographs or samples of wear, Pickup, Chipping, or breakage;
- regrinding and recoating expectations;
- Erforderliches Material, Härte, dimensional, oder Beschichtungsdokumentation.
SunshinePro states that it supplies standard components and non-standard customized parts processed from customer drawings. Its relevant punch pages list combinations of CNC machining, Präzisionsschleifen, EDM, Vakuumwärmebehandlung, custom dimensions, HSS, Hartmetall, stainless tool steel, and selected coating options.
These website-confirmed capabilities should still be reviewed against the actual drawing and application. A tolerance or material listed on one product page should not be assumed to apply to every punch geometry.
Endgültiges Auswahlprinzip
Use this order when selecting punch pins for stainless steel stamping:
- Identify the stainless grade, Zustand, Dicke, and feature geometry.
- Determine whether the current failure is galling, Abrasiver Verschleiß, Chipping, Bruch, oder Deformation.
- Correct alignment, Freigabe, Anleitung, Finish, Stripping, and lubrication problems.
- Select the substrate for bulk toughness, Druckfestigkeit, and edge stability.
- Select the coating or treatment for the dominant surface failure.
- Compare serviceability, Ausfallzeit, and cost per hit.
- Confirm the final system through drawing review and application-specific validation.
For a custom review, Reichen Sie die Zeichnung ein, stainless specification, Produktionsbedingungen, and current failure details through SunshinePro’s Kontaktseite. That information gives the supplier a practical basis for evaluating the punch material, Wärmebehandlung, Finish, Beschichtung, und Inspektionsanforderungen.
Freigeben:



Geschrieben von Sunshine
Bei Sunshine, Wir sind ein professioneller Hersteller und Lieferant von Präzisionsformkomponenten, bietet ein breites Produktsortiment für Stange- und Spritzgussanwendungen. Unser Kernfokus liegt auf dem Stanzen von Stempeln, Auswurfstifte und -hülsen, sowie Führungspfosten und Buchsen. Mit fortschrittlicher CNC-Bearbeitung, Strenge Qualitätskontrolle, und starke Produktionskapazitäten, Wir sorgen für Zuverlässigkeit, Hochpräzisionsteile, zusammen mit vorrätigen Standardkomponenten für schnelle und effiziente weltweite Versorgung.
NACHRICHTEN
EMPFANG SERVICE
Mit hochwertigen Teilen für jedes Budget und freundlichem Personal, das geschult ist, um Ihren Besuch informativ und unkompliziert zu gestalten.
