



Lochstift-Inspektionscheckliste für eingehende und routinemäßige Qualitätskontrolle
A punch pin inspection checklist should answer four questions: Is this the correct punch? Does it match the approved specification? Is it still fit for service? What action should follow the inspection?
This guide covers individual punch pins used in metal-stamping dies. Incoming QC verifies a newly supplied punch against the purchase order, Zeichnung, revision, and required documentation. Routine QC checks whether a punch remains serviceable after production use, Nachschleifen, a collision, or another abnormal event.
Punch pins work within a larger die system. Guides, Buchsen, retainers, stripper components, die clearance, and alignment can all influence punch condition. The broader roles of these components are covered in the Leitfaden für die Stanzenkomponenten (Schlussfolgerung). Hier, the focus stays on inspecting and dispositioning the punch pin itself.
No universal tolerance, inspection interval, or wear limit applies to every punch pin. Acceptance must be based on the approved drawing, purchase specification, control plan, or another documented requirement.
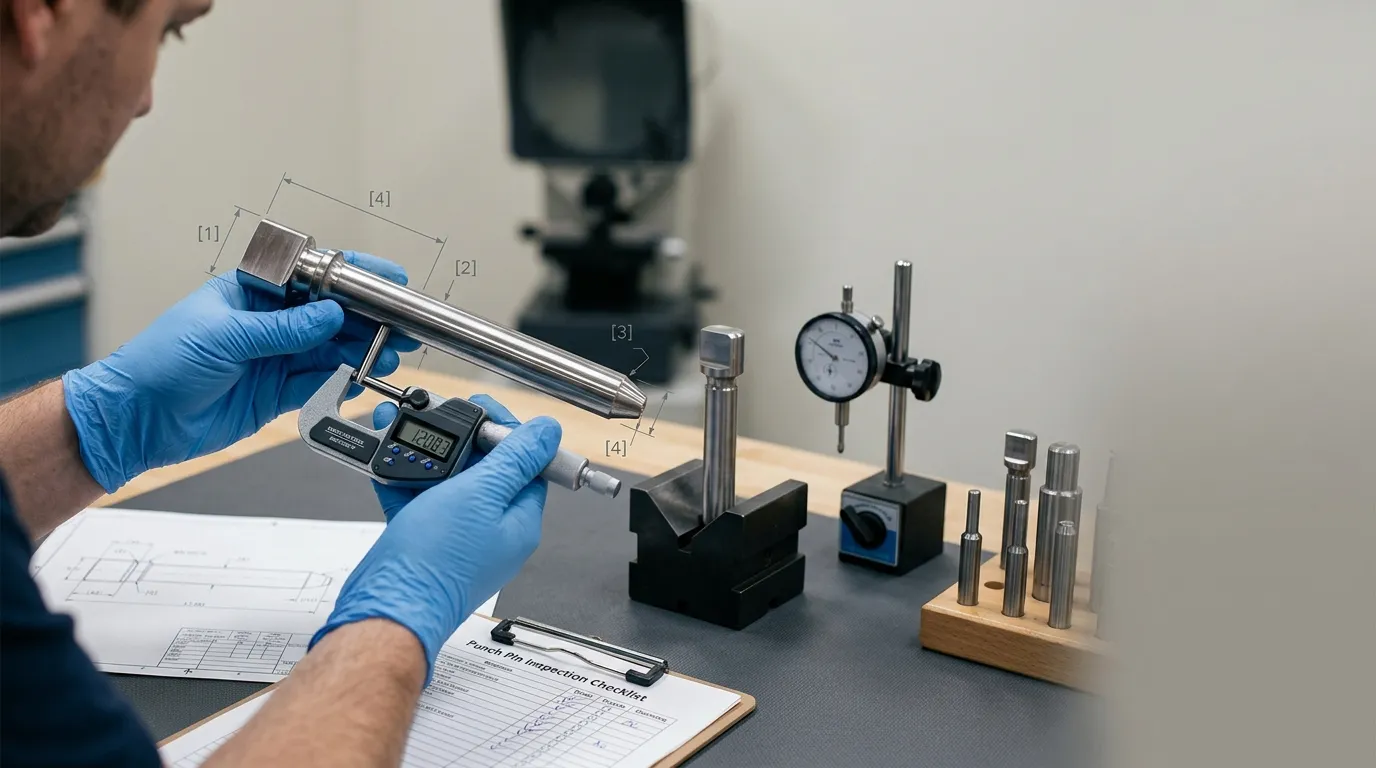
Eingehende Qualitätskontrolle und routinemäßige Qualitätskontrolle prüfen unterschiedliche Risiken
Incoming and routine inspection use many of the same instruments, but they answer different questions.
| Inspektionsphase | Hauptzweck | Typische Prüfungen | Hauptentscheidung |
|---|---|---|---|
| Eingehende QC | Bestätigen Sie, dass der gelieferte Stanzer der Bestellung und der genehmigten Spezifikation entspricht | Part identity, Zeichnungsrevision, material or coating documents, visible damage, Abmessungen, Geometrie, inspection report | Annehmen, hold, return, or reject |
| Routinemessige Qualitätskontrolle | Bestätigen Sie, dass ein gebrauchter Stempel sicher und funktionsfähig bleibt | Kantenverschleiß, Risse, Ärger, Dimensionsänderung, Runout, Arbeitsdauer, Produktionssymptome, regrind history | Rückkehr in den Dienst, Monitor, regrind, Ersetzen, or investigate |
| Nach-Nachmahl-Inspektion | Bestätigen Sie, dass das Schärfen die Kante wiederherstellt hat, ohne andere Merkmale unzulässig zu machen. | Edge form, burr removal, Gesamtlänge, Arbeitsdauer, Profil, Oberflächenzustand | Release, Überarbeitung, oder ersetzen |
| Nachkontrolle nach dem Event | Check for hidden or visible damage after a jam, Kollision, misfeed, or nearby breakage | Risse, Biegen, head damage, Runout, Sitzflächen, Koppelkomponenten | Quarantäne, Untersuchen Sie, Reparatur, oder ersetzen |
Incoming inspection should establish a reliable baseline. Recording the punch’s as-received dimensions and condition makes later wear easier to identify.
Routine inspection compares the current punch against that baseline and any approved service limits. A punch can remain within its original manufacturing tolerance yet show an abnormal wear trend. Umgekehrt, a worn feature may still appear visually acceptable while no longer meeting the documented service requirement.
Prepare the Punch, Dokumente, and Measuring Equipment
Inspection should not begin with a caliper. It should begin with the correct documents, part identity, and measurement conditions.
- Confirm the inspection stage. Record whether the punch is incoming, in routine service, newly reground, or being checked after an abnormal event.
- Obtain the approved drawing. Verify the drawing number and revision before measuring anything. An accurate measurement against an obsolete revision is still an invalid inspection result.
- Review the purchase and quality requirements. Check the purchase order, control plan, approved sample, inspection-report requirement, and any requested material, Wärmebehandlung, Härte, or coating documentation.
- Match the punch to its records. Confirm the part number, lot or serial number, Menge, material designation, coating designation, and any engraved identification.
- Inspect the packaging before cleaning. Record impact damage, Korrosion, broken protective packaging, loose punches, or signs that sharp edges contacted each other during transport.
- Clean the punch carefully. Entfernen Sie das Öl, Dreck, Chips, and transferred material without rounding the cutting edge or scratching a coated surface. Residue on a diameter or seating face can affect the measurement.
- Stabilize the part when tolerances are tight. A punch arriving from a hot production area, cold warehouse, or vehicle may need time to reach the inspection environment. Temperature differences can affect dimensional results.
- Verify the measuring equipment. Check instrument identification, calibration status, measuring range, Auflösung, Kontaktbedingung, and cleanliness. Confirm that any V-block, Zentrum, Spielplan, or surface plate is also clean and suitable for the feature.
SunshinePro states that non-standard mold parts can be processed from customer drawings, while its punch-pin page lists diameter, Länge, Kopfstil, Materialqualität, and coating as customizable characteristics. Those fields should therefore be treated as drawing- and order-specific requirements rather than assumed product defaults.
Widersprüchliche oder fehlende Spezifikationen vor der Messung beheben
Do not select a tolerance from memory, an old inspection sheet, or a generic catalog.
Place the punch on hold when:
- the drawing revision does not match the purchase order;
- the inspection report refers to another part or lot;
- the drawing and purchase specification contain conflicting limits;
- the material or coating designation is missing;
- the required datum or measurement method is unclear;
- an approved deviation is mentioned but not supplied.
Obtain written clarification from the responsible engineer, customer, or supplier before assigning a pass or fail result. The controlling-document hierarchy should follow the customer’s quality system or contract rather than an informal assumption.
Überprüfen Sie jede Stempelfunktion auf sichtbare Schäden
Visual inspection is the fastest way to find obvious defects, but it should follow a consistent feature-by-feature sequence.
Use clean lighting and suitable magnification. Rotate the punch and inspect the complete circumference rather than viewing only one side.
| Inspektionszone | Bedingungen zu überprüfen | Mögliche Bedeutung | Typische nächste Aktion |
| Schneide und Spitze | Chipping, Risse, Kantenrundung, Mahlscheiben, Verformung, Pickup | Loss of cutting quality, Lokale Überlastung, Auswirkungen, Verschleiß, adhesive material transfer | Maß, quarantine, regrind, oder ersetzen |
| Schaft oder Körper | Punktewertung, Ärger, wear bands, Korrosion, Nerven, Übertragenes Material | Poor guidance, Reibung, Fehlstellung, lubrication problem, Falsche Passung | Sauber, measure diameter/runout, inspect mating parts |
| Kopf und Schulter | Pilzbildung, Peening, Risse, uneven seating marks, Verformung | Überlastung, incorrect seating, retainer problem, unzureichende Unterstützung | Quarantäne und Inspektion des Zustands der Bedienung oder der Sitzordnung |
| Übergangsradien | Risse, grinding marks, abrupt surface changes | Spannungskonzentration, Grindschaden, fatigue initiation | Magnify, escalate, oder ersetzen |
| Beschichtete Oberfläche | Peeling, Abblättern, Kratzer, Verfärbung, freiliegendes Substrat | Coating damage, Reibung, Auswirkungen, Korrosion, Verschleiß | Record location, assess function, seek engineering review |
| Identifikationsmerkmale | Missing or illegible part, lot, or serial information | Verlust der Rückverfolgbarkeit oder Risiko der Vermischung von Überarbeitungen | Warten, bis die Identität bestätigt ist |
A small chip at the cutting edge is not equivalent to a superficial scratch on a non-working surface. The inspection record should state the defect location, approximate extent, and whether it affects a functional feature.
Risse, Schwere Verformung, or a damaged retention head generally justify immediate quarantine. Galling, Pickup, or one-sided scoring may require inspection of the die system as well as the punch. Detailed causes of cracking and catastrophic failure belong in the guide to Stanzbruch in Stempelwerkzeugen.
Was die Sichtprüfung nicht bestätigen kann
Visual inspection cannot reliably establish:
- exact body or tip diameter;
- overall or working length;
- Geradlinigkeit;
- Runout, Konzentrizität, or coaxiality;
- shaped-tip profile;
- numerical surface roughness;
- Materialqualität;
- heat-treatment conformity;
- Härte;
- coating identity.
A punch may look undamaged but still be dimensionally out of tolerance. Materialqualität, Härte, and coating conformity may require traceable documentation or a specified test method.
Messen Sie die Maße und Geometrie, die Passung und Funktion steuern
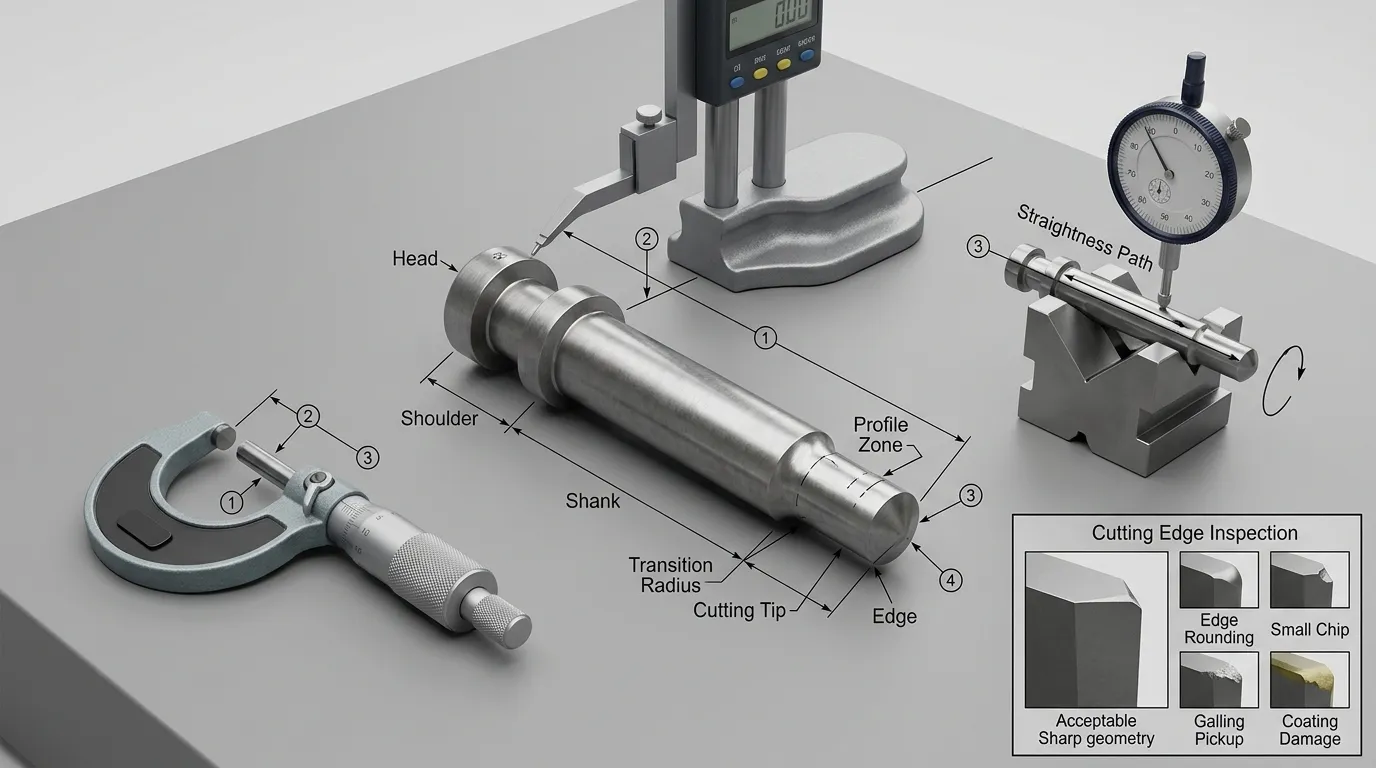
The approved drawing determines which dimensions and geometric controls must be inspected. Not every punch requires every measurement.
| Charakteristik | Warum es wichtig ist | Mögliche Messmethode | Erhebliche Einschränkung | Akzeptanzquelle |
| Körper- oder Schaftdurchmesser | Affects guidance, Passform, Verbleib, und Ausrichtung | Outside micrometer; suitable limit gauge | Kontaktort und Taper müssen berücksichtigt werden | Zeichnungs- oder Passspezifikation |
| Spitzendurchmesser | Beeinflusst die Größe der durchbohrten Merkmale und die Beziehung zwischen Stanzen und Stanzen | Mikrometer, specialized gauge, optical system | Kleine oder empfindliche Spitzen eignen sich möglicherweise nicht für Standardkontaktlinsen | Zeichnung |
| Geformtes Spitzenprofil | Kontrolliert nicht-runde Löcher oder geformte Geometrie | Optical comparator, vision system, CMM | Erfordert korrekte Referenzausrichtung und Profilinterpretation | Zeichnung mit Profilanforderung |
| Gesamtlänge | Supports identification, installation, and regrind tracking | Height gauge, micrometer, Komparator, dedicated fixture | Sitzflächen müssen sauber und konsequent referenziert sein | Zeichnung |
| Arbeitslänge oder Projektion | Einflüsse auf Betriebsposition und Durchschlag | Height gauge, Komparator, dedicated inspection fixture | Definition must match the drawing; do not borrow tablet-tooling terminology | Zeichnungs- oder Aufbauspezifikation |
| Kopfdurchmesser und -dicke | Beeinträchtigt die Behalten und Sitzplatzierung | Mikrometer, caliper for screening, Komparator | Mahlwerke oder Peening können den Kontakt verzerren | Zeichnung |
| Schulterposition | Einflüsse: Sitzplätze und zusammengesetzte Projektion | Height gauge, Komparator, CMM | Die Begrenzungseinrichtung muss die Zeichnungsanforderung reproduzieren | Zeichnung |
| Geradlinigkeit | Erkennt Biegungen oder Achsenabweichungen | Indicator with suitable support, CMM, dedicated fixture | Unterstützungsmethode und Datumswahl beeinflussen das Ergebnis | Zieh- oder genehmigtes Dienstlimit |
| Kreisförmiger oder vollständiger Auslauf | Zeigt die Rotationsvariation relativ zu einer Bezugsachse | Indicator with centers or V-block; CMM | "Runout" muss exakt mit der Ziehkontrolle übereinstimmen | Zeichnung |
| Konzentrizität oder Koaxialität | Bewertet die Beziehung zwischen Achsen oder Merkmalen | CMM oder anerkannte spezialisierte Methode | Ersetzen Sie keinen einfachen Runout-Check, es sei denn, der Ingenieur genehmigt ihn | Zeichnung |
| Senkrecht | Beeinflusst die Sitzordnung oder Ausrichtung der Endflächen und Schultern | Indicator, surface plate setup, CMM | Erfordert eine gültige Bezugsreferenz | Zeichnung |
| Oberflächenrauheit | Can influence friction, Passform, Veröffentlichung, and galling | Oberflächenrauheitsprüfer | Parameter, Cutoff, Regie, and location must be specified | Zeichnung oder Oberflächenspezifikation |
| Härte | Kann eine Wärmebehandlungsanforderung bestätigen | Genehmigter Härtetest oder Lieferantendokumentation | Test scale, Lage, Oberflächenzustand, and indentation effect matter | Zeichnung oder Materialspezifikation |
Geometric terms should be interpreted according to the drawing standard in use. ISO 1101 defines geometrical tolerancing concepts in the ISO system, während ASME Y14.5 is widely used for US-oriented GD&T drawings.
A drawing that specifies runout should not be rewritten as concentricity during inspection. These controls describe different requirements and may require different measurement strategies.
SunshinePro’s tungsten-carbide punch page lists micrometer or caliper checks, projector measurement, and roughness testing for that product category. Those published methods show the types of inspection that may be relevant, but they do not prove that every punch or every order receives the same checks.
Wählen Sie das Instrument entsprechend der Toleranz und dem Merkmal aus
Instrument choice should be based on the feature, Toleranz, Zugang, and required measurement confidence.
| Instrument | Bester Einsatz | Hauptbegrenzung |
| Mikrometer | Zugängliche äußere Durchmesser und Dicken | Contact geometry may not suit small, Konisch, delicate, or irregular features |
| Sattel | Identification, broad dimensions, and screening | Auflösung und Operator-Einfluss können für enge Toleranzen ungeeignet sein |
| Höhenanzeige und Oberflächenplatte | Axial dimensions, shoulder positions, and comparative height checks | Erfordert kontrollierte Sitz- und Begrenzungseinrichtung |
| Zifferblattanzeiger mit V-Block oder Centern | Runout, rotational variation, and some straightness checks | Die Ergebnisse hängen stark von der Stützposition und der Referenzsimulation ab |
| Optischer Komparator oder Visionssystem | Profiles, Winkel, Radien, tip shapes, and edge form | Requires alignment, magnification control, and correct profile interpretation |
| CMM | Komplexe Geometrie und datumbasierte Beziehungen | Probe access, Ausstattung, strategy, and uncertainty must be controlled |
| Go/No-Go-Anzeige | Schnelle funktionale Verifikation einer Größenbegrenzung | Es gibt Bestanden/Nicht-bestehende Informationen, aber nicht die tatsächliche Abweichung oder den Verschleißtrend |
| Rauheitstester | Numerische Oberflächentexturverifikation | Requires the correct parameter, Regie, Cutoff, and measurement location |
Einfache Grenzmessinstrumente werden abgedeckt durch ISO 1938-1. A go/no-go gauge can be efficient for repeated checks, but variable measurement is still useful when the actual size or rate of wear matters.
Surface-texture requirements should be read from the drawing rather than inferred from appearance. ISO 21920-1 covers the indication of profile surface texture in technical product documentation.
Entscheide, ob das Ergebnis akzeptabel ist
A measured value is not meaningful until it is compared with an approved requirement.
Possible acceptance sources include:
- the current approved drawing;
- the purchase specification;
- the control plan;
- an approved customer deviation;
- an approved sample with defined measurement criteria;
- a documented service limit;
- a validated internal wear limit.
Nominal size alone does not determine acceptance. A drawing dimension of 10 mm, Zum Beispiel, cannot be judged without its tolerance and any related geometric or surface requirements.
Use a controlled decision process:
| Ergebnisbedingung | Erforderliche Antwort |
| Das liegt eindeutig im Rahmen der Anforderung | Das Ergebnis aufzeichnen und den Stempel akzeptieren oder in den Dienst zurückgeben |
| Nahe an einer Grenze oder inkonsistent | Verify cleanliness, Temperatur, instrument, method, Ausstattung, datum setup, und Wiederholbarkeit |
| Außerhalb der Anforderung | Quarantäne den Stempel absetzen und den genehmigten Nicht-Konformitätsprozess starten |
| Die Spezifikation fehlt oder es ist ein Konflikt | Halte die Stanz zurück, bis eine schriftliche Klarstellung eingegangen ist |
| Wiederholter Defekt nach Austausch oder Nachschleifen | Untersuchen Sie die größeren Stanzensystem- und Prozessbedingungen |
Measurement uncertainty becomes important near a specification limit. ISO 14253-1 provides decision rules for proving conformity or nonconformity while accounting for measurement uncertainty.
In practical terms, a borderline reading should not be accepted or rejected casually. Confirm that the instrument and method are capable of resolving the requirement, then apply the organization’s documented decision rule.
Probenahmen oder 100%ige Inspektionen hängen vom Risiko und den Vertragsanforderungen ab
The inspection quantity should be determined by:
- customer or contract requirements;
- characteristic criticality;
- lot size;
- supplier performance history;
- process capability;
- failure consequence;
- previous nonconformities;
- whether the result is needed for wear trending;
- the control plan.
A statement such as “100% inspected” should identify which characteristics were checked. It may mean every punch received an identification and visual check, while only selected pieces received complete dimensional inspection.
Go/no-go gauging may support rapid inspection of every piece, but it does not provide the variable data needed to evaluate size distribution or wear trends.
Verwenden Sie eine routinemäßige Inspektion, um den Verschleiß vor dem Ausfall zu überprüfen
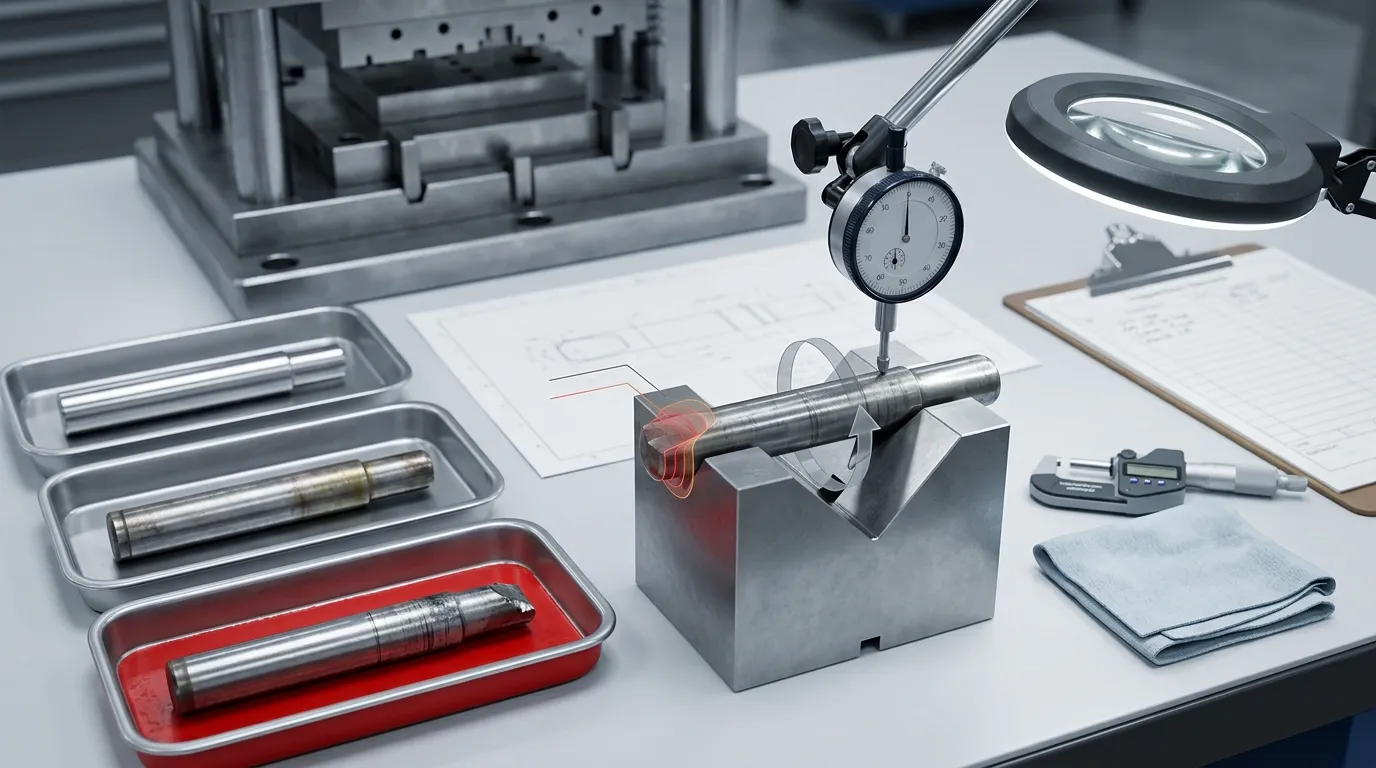
Routine QC should be based on risk and production history rather than one fixed interval for every punch.
Establish a baseline when the punch is first accepted, approved after setup, or returned from regrinding. Record dimensions and visible condition for the features most likely to change.
Trigger inspection when any of the following occurs:
- a planned production or maintenance interval is reached;
- the punch completes a high-risk or high-volume run;
- burr height or edge quality changes;
- stamped dimensions begin to drift;
- scratching or pickup appears on the part;
- stripping force increases;
- press load or operating sound changes;
- slug pulling or jamming occurs;
- a misfeed, Kollision, or material double-feed occurs;
- a nearby punch chips or breaks;
- the tool is removed for maintenance;
- Schmierung, stock material, or process settings change;
- the punch returns from regrinding.
Compare current values with the baseline and approved service limits. Trend data can reveal gradual wear before a dimension crosses a rejection limit.
Production symptoms should be treated as inspection triggers, Keine automatischen Diagnosen. Burrs may result from a worn punch, but they can also reflect die wear, Freigabe, Ausrichtung, work-material variation, or stripper problems. Das Leitfaden für Stanzenwerkzeuge provides broader context on die materials, Toleranzen, Freigabe, and system-level tooling considerations.
Überprüfen Sie den Stempel erneut nach dem erneuten Schleifen oder einem ungewöhnlichen Ereignis
A sharp edge does not by itself prove that a reground punch is ready for service.
Nach dem Nachschleifen, prüfen:
- cutting-edge form;
- burr-free condition;
- Gesamtlänge;
- working length or projection;
- tip diameter or profile;
- surface damage or overheating;
- remaining regrind allowance, where documented;
- identification and regrind history.
After a collision, misfeed, jam, or nearby breakage, also check:
- Risse;
- permanent bending;
- head or shoulder deformation;
- Runout;
- Sitzflächen;
- guide and retainer contact;
- the mating die opening and surrounding components.
Do not return a punch to service solely because no visible crack is present. A collision can change alignment or runout without producing an obvious surface defect.
Zeichnen Sie das Ergebnis auf und weisen Sie eine kontrollierte Disposition zu
Inspection records should identify the punch, the requirement, the method, the result, and the final decision.
Mindestens, Aufzeichnung:
- Teilenummer;
- Zeichnungsnummer und Überarbeitung;
- Lieferant;
- purchase order;
- lot or serial number;
- material and coating designation;
- inspection stage;
- characteristic inspected;
- specification and tolerance;
- measured result;
- instrument identification;
- inspector;
- inspection date;
- disposition;
- Anmerkungen, photographs, or defect location where useful.
Use a controlled disposition rather than an informal “looks okay” decision.
| Funde | Mögliches Layout |
| Alle erforderlichen Eigenschaften entsprechen | Akzeptieren oder in den Dienst zurückkehren |
| Das Ergebnis ist inkonsistent oder nahe an einer Grenze | Sauber, stabilize, remeasure, or verify with a more capable method |
| Die Dokumentation fehlt | Halten oder in Quarantäne, bis Beweise vorgelegt sind |
| Reparierbarer Kantenverschleiß innerhalb einer genehmigten Genehmigung | Lassen Sie das von der Ingenieur genehmigte Nachschleifen anfordern |
| Crack, Starke Absplitterungen, permanent bending, or unsafe head damage | Ersetzen oder ablehnen |
| Die Dimension liegt außerhalb der Anforderung | Quarantäne und Prozess als nichtkonform |
| Der gleiche Schaden tritt wiederholt auf | Investigate clearance, Ausrichtung, Anleitung, Verbleib, Schmierung, und Prozessbedingungen |
Nonconforming punches should be clearly identified and physically segregated so they cannot return to production accidentally.
SunshinePro states that its quality approach includes raw-material inspection, In-Prozess-Überwachung, Endgültige Tests, measuring equipment, and inspection reports. Buyers should still define the required inspection characteristics and documentation for each order rather than assume that one standard report fits every punch.
Was man von einem Stanzstift-Lieferanten anfordern sollte
A buyer should define inspection evidence before the order is released, especially for custom or critical punches.
Request the items that are relevant to the application:
- genehmigte Zeichnung und Überarbeitung;
- part, lot, and serial identification requirements;
- drawing-specific inspection report;
- material certificate or certificate of conformity;
- heat-treatment or hardness evidence where specified;
- coating documentation where specified;
- Genehmigte Abweichungen;
- packing and corrosion-protection requirements;
- identification of characteristics receiving 100% inspection;
- identification of characteristics inspected by sampling;
- measurement method for tight or complex tolerances;
- traceability between the punch, certificate, and inspection report.
Broad catalog statements are not a substitute for characteristic-level evidence. A supplier may state a general tolerance capability, but the buyer still needs confirmation that the required feature, Material, Geometrie, and measurement method are suitable for the specific drawing.
SunshinePro lists tool steel, Hochgeschwindigkeitsstahl, Hartmetall, CNC-Bearbeitung, Präzisionsschleifen, EDM, Vakuumwärmebehandlung, and drawing-based customization on its punch-related pages. These published options can support an RFQ discussion, but the exact material, Ablauf, Toleranz, Beschichtung, and inspection documentation should be confirmed for the individual part.
Zusammenfassung der Lochstift-Inspektionscheckliste
Use this condensed sequence for incoming, routine, post-regrind, and post-event inspections:
- Identify the inspection stage.
- Confirm the part number, lot or serial number, Zeichnung, and revision.
- Review the purchase order, control plan, and document requirements.
- Inspect packaging and record transport damage.
- Clean the punch without damaging its edge or coating.
- Verify instrument condition, range, Auflösung, and calibration status.
- Inspect the cutting edge, Hinweis, Karosserie, Kopf, Schulter, Radien, Beschichtung, and identification.
- Measure the dimensions and geometric characteristics required by the drawing.
- Use an instrument suitable for the feature and tolerance.
- Compare results with the approved acceptance source.
- Verify borderline results and account for measurement uncertainty.
- Record the specification, result, instrument, inspector, und Datum.
- Annehmen, hold, quarantine, regrind, Ersetzen, or reject through a controlled disposition.
- Investigate the wider die system when the same damage repeatedly returns.
For a custom or replacement punch, submit the approved drawing together with the required material, Beschichtung, Inspektion, and documentation needs. SunshinePros Die Punch Pin page provides its published product context, und die Kontaktseite can be used to request drawing review or clarify inspection-report requirements.
Freigeben:



Geschrieben von Sunshine
Bei Sunshine, Wir sind ein professioneller Hersteller und Lieferant von Präzisionsformkomponenten, bietet ein breites Produktsortiment für Stange- und Spritzgussanwendungen. Unser Kernfokus liegt auf dem Stanzen von Stempeln, Auswurfstifte und -hülsen, sowie Führungspfosten und Buchsen. Mit fortschrittlicher CNC-Bearbeitung, Strenge Qualitätskontrolle, und starke Produktionskapazitäten, Wir sorgen für Zuverlässigkeit, Hochpräzisionsteile, zusammen mit vorrätigen Standardkomponenten für schnelle und effiziente weltweite Versorgung.
NACHRICHTEN
EMPFANG SERVICE
Mit hochwertigen Teilen für jedes Budget und freundlichem Personal, das geschult ist, um Ihren Besuch informativ und unkompliziert zu gestalten.
