



Stempelbolzen für progressive Stempel: Präzision für Hochzykluswerkzeuge
Punch pins for progressive dies must be selected as part of a complete station system, not as isolated hardened components. The operation performed at the station, strip material, feature geometry, cutting clearance, punch support, Ausrichtung, Stripping-Bedingungen, and maintenance plan all affect punch reliability.
A harder material or premium coating cannot compensate for excessive unsupported length, Schlechte Ausrichtung, Falsche Freigabe, or unstable strip feeding. Für umfassendere Informationen zu Stempeltypen, Materialien, Toleranzen, und Beschaffung, Siehe die Leitfaden für Stanzenwerkzeuge (Schlussfolgerung). This guide focuses specifically on selecting, diagnosing, and specifying working punches for progressive tooling.
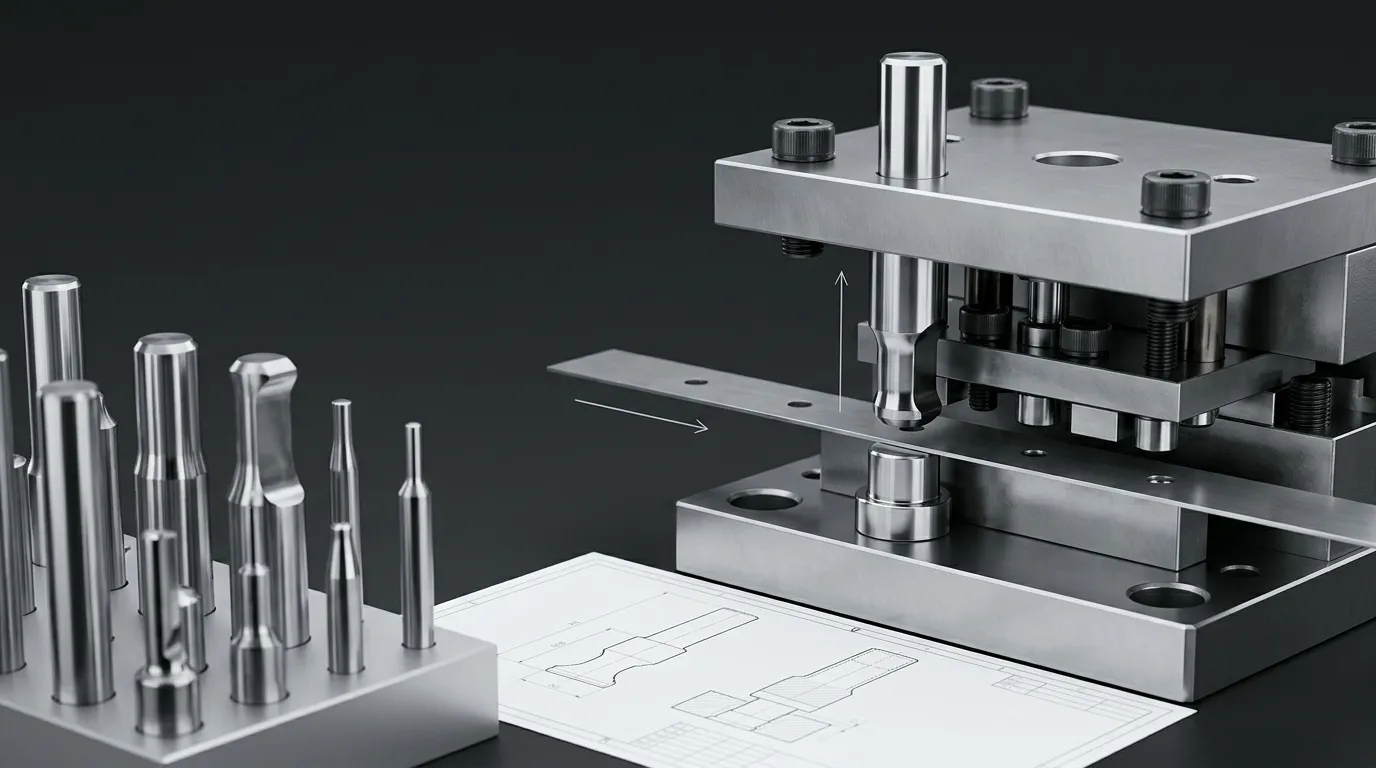
Warum progressive Stempel stationsspezifische Stanzspezifikationen benötigen
A progressive die moves strip material through a sequence of stations. Each press stroke may pierce, notch, trim, Form, or separate a feature while the feeder and pilots maintain the strip’s position.
This creates several demands that are less significant in a simple single-operation die:
- Errors at one station can affect every station that follows.
- Repeated side loading can gradually deflect a punch even before visible failure occurs.
- Feed or pilot errors can move the strip relative to the punch.
- Stripping force loads the punch during withdrawal from the stock.
- Slugs or loose material can interfere with later operations.
- Regrinding one punch can alter penetration or timing relative to other stations.
“High-cycle” therefore describes an operating condition, not a guaranteed number of strokes. Actual punch life depends on the complete combination of material, Geometrie, Freigabe, Pressebedingungen, Schmierung, Unterstützung, und Wartung.
Stimmen Sie den Stempel an die Operation an jeder Station an
The first selection question should be: What does this punch do at its station?
Different operations create different loading patterns.
| Stationsbetrieb | Hauptnachfrage nach Punch | Häufige Risiken zu bewerten |
|---|---|---|
| Piercing | Wiederholtes Scheren durch ein geschlossenes Profil | Kantenverschleiß, small-section breakage, slug pulling, Gratwachstum |
| Kerben oder Trimmen | Scherung entlang eines Streifenrandes oder einer teilweisen Kontur | Asymmetric load, side deflection, ungleichmäßiger Verschleiß |
| Cutoff | Endgültige Trennung des Bauteils oder Trägers | High separation load, timing sensitivity, Schock |
| Bildung | Plastische Verformung statt einfacher Scherung | Side thrust, Materialfluss, Ärger, profile wear |
| Piloting | Streifenregistrierung statt Merkmaleschnitt | Position error, pilot entry damage, feed mismatch |
A small round piercing punch, Zum Beispiel, may be limited by slenderness and slug behavior. A long trimming profile may be more sensitive to uneven loading across its edge. A forming punch may need greater resistance to lateral force and material pickup.
Arbeitsstempel und Pilotbolzen erfüllen unterschiedliche Aufgaben
A working punch cuts or forms the strip. A pilot pin enters a previously produced hole or locating feature to refine strip position before critical operations occur.
The terms are sometimes mixed in supplier catalogues, so the drawing and RFQ should state the function clearly. Die ISO 8695 Stempelterminologie-Standard can help distinguish recognized punch types, while pilot design still needs to reflect strip thickness, feed conditions, and the actual locating method.
A pilot should not be selected using the same assumptions as a piercing punch. Its entry shape, Lage, Freigabe, and relationship with the feeder are central to its function.
Specify Geometry, Unterstützung, and Alignment as One System
Punch geometry cannot be evaluated only by nominal diameter or overall length. The designer must consider the smallest working section, profile transitions, Shank, Kopf, Nicht getragene Länge, retention method, and mating die opening.
For a reliable specification, Rezension:
- working-tip diameter or profile;
- smallest cross-section;
- unsupported length below the guide or holder;
- shank and head dimensions;
- transition radii where the part design allows them;
- straightness and relevant runout;
- concentricity between the working end and shank;
- profile tolerance for non-round punches;
- edge condition and regrind allowance;
- functional datums for replacement inspection.
A punch that is strong in compression can still fail if it is long, schlank, poorly guided, or exposed to lateral load.
Profil und nicht unterstützte Längen-Kontrollstanzsteifigkeit
As unsupported punch length increases, resistance to deflection decreases. Narrow slots, small diameters, sharp profile changes, and asymmetric cutting edges further increase stress concentration.
Side loading is especially damaging because it can move the punch tip away from the intended axis. This changes the effective clearance around the profile. One side may then carry more cutting load, causing uneven wear or local chipping.
Technische Leitlinien zu Verbesserung der Lebensdauer des Schlages also connects lateral loading with punch-tip deflection and altered cutting clearance. This is why repeated breakage should not automatically lead to a harder punch material. The underlying problem may be geometry, Unterstützung, feed position, or station loading.
The Holder, Backing Plate, Stripper, and Die Button Must Agree
The punch operates through a stack of supporting components:
| Komponente | Beziehung zum Punsch | Probleme, wenn die Beziehung schlecht ist |
| Stempelhalter oder Retainer | Findet und sichert den Schaft | Position error, Lockerheit, repeated misalignment |
| Rückplatte | Unterstützt den Lochkopf unter axialer Last | Head indentation, Schlechte Sitzplätze, local overload |
| Stripper-Platte | Entfernt den Stock und kann das Arbeitsende lenken | High withdrawal load, tip movement, Punktewertung |
| Würfelknopf oder Matrix | Nimmt den Stempel entgegen und legt die Schneidöffnung fest | Ungleichmäßige Räumung, Kantenschaden, Gratvariante |
| Führpfosten und Buchsen | Halten Sie die Ausrichtung von Ober- zu Unter-Chips bei. | Off-center entry, Einseitige Abnutzung, Chipping |
A guided stripper can help maintain the punch tip’s relationship with the die opening. MISUMIs technische Erklärung der Matrixstrukturen notes the use of movable strippers for precision and progressive punching, including punch-tip guidance.
The wider roles of holders, backing plates, Stripperinnen, die buttons, and guide systems are covered in the Leitfaden für die Stanzenkomponenten. For this application, the important point is that changing only the punch may not solve a support or alignment problem.
Control Clearance, Strip Registration, and Slug Movement
The punch and die opening form a working pair. Their relationship affects cutting load, fracture behavior, Burr-Formation, Kantenverschleiß, und Slug-Bewegung.
Clearance should be based on the actual:
- Werkstücksmaterial;
- strip thickness;
- hardness or strength;
- feature geometry;
- erforderliche Kantenbedingung;
- punch and die material;
- alignment capability;
- expected wear behavior.
A nominal clearance value is not enough if the punch deflects or the die set is misaligned. The effective clearance may become larger on one side and smaller on the other.
Die Freigabe muss dem Material und dem Merkmal entsprechen
There is no single clearance percentage suitable for every progressive-die station.
Research on blanking has shown that clearance can influence punch wear, burr size, and the geometry of the cut feature. Eins Peer-reviewte Studie zu gehärtetem Stahlblech found measurable relationships among blanking clearance, Stanzverschleiß, and burr development under its tested conditions.
The practical lesson is not to copy the study’s values into an unrelated die. Instead, use the material grade, Dicke, Stärke, Geometrie, and quality requirement to establish a starting condition, then verify it through controlled inspection.
Uneven wear around the punch should trigger checks for:
- off-center punch entry;
- worn guide components;
- punch deflection;
- die-button movement;
- feeder or pilot error;
- uneven cutting load;
- local edge damage.
Registrierung und Slug-Kontrolle schützen stromabwärts gelegene Stationen
Progressive tooling depends on repeatable strip positioning.
A typical sequence is:
- The feeder advances the strip by the intended pitch.
- Pilots refine or confirm strip position.
- The stripper controls the stock near the working area.
- The punch enters the strip and die opening.
- The slug or trimmed material clears the station.
- The stripper removes the stock from the punch during return.
A feed or pilot problem can cause the punch to engage the strip off-center. Excessive stripping force can bend a slender punch or loosen its retention. A returned slug can remain on the punch face, re-enter the strip, or interfere with a later station.
Slug pulling therefore should not be treated only as a waste-removal issue. It can become a punch-damage and strip-progression problem.
Wähle Material und Beschichtung nach dem dominanten Versagensrisiko
Punch material should be selected after identifying the expected loading and failure mode. Maximum hardness alone is not a reliable selection method.
The main properties to balance are:
- Verschleißfestigkeit;
- Zähigkeit;
- Druckfestigkeit;
- resistance to plastic deformation;
- dimensional stability after heat treatment;
- resistance to chipping under shock or side load;
- suitability for the intended coating and finish.
Wählen Sie das Substrat vor der Beschichtung aus
| Anwendungszustand | Materialrichtung zur Bewertung | Hauptbeschränkung zur Überprüfung |
| Mäßiger Verschleiß bei Aufprall oder variabler Belastung | Kategorie Werkzeugstahl oder Hochgeschwindigkeitsstahl | Kann schneller verschleißen als eine widerstandsfähigere Variante |
| Starker abrasiver Verschleiß mit stabiler Ausrichtung | Higher-wear tool steel, powder-metallurgy steel, oder Karbid | Kosten, Schleifen, Chipping, and support requirements |
| Kleiner Stempel mit wiederholter seitlicher Last | Härterer Stahl und verbesserte Führung | Der Verschleiß kann zunehmen, wenn das Substrat zu weich ist |
| Stable, high-wear piercing condition | Karbid kann in Betracht gezogen werden | Sensitive to shock, Fehlstellung, and inadequate support |
| Klebstoffverschleiß oder Aufnahme | Suitable substrate plus finish, Schmierung, or coating review | Die Beschichtung kann keine Geometrie- oder Freistandsfehler korrigieren |
Carbide can provide high wear resistance and compressive strength, but it is not automatically the best choice for every station. A carbide punch exposed to misalignment, Schock, or side loading may chip where a tougher steel would tolerate the same disturbance.
SunshinePro listet SKH51, SKH9, DC53, ASP grades, and carbide among its punch-pin material categories. These are available directions, not proof that one grade is suitable for a specific die. The final choice requires the work material, Geometrie, Unterstützung, Produktionsbedingungen, und Ausfallgeschichte.
Verwendung von Beschichtungen für ein definiertes Oberflächenproblem
A coating should target a known surface issue such as abrasive wear, Haftverschleiß, Ärger, oder Materialaufnahme.
Before selecting one, Bestätigen:
- punch substrate and heat treatment;
- surface finish before coating;
- coating adhesion requirements;
- workpiece material and surface condition;
- Schmierung;
- Betriebstemperatur;
- whether the punch will be reground;
- whether the coated surface includes the cutting edge, sidewall, oder beides.
SunshinePro listet TiN auf, TiCN, and DLC as custom punch-pin coating options. The appropriate choice depends on the substrate and contact conditions. No coating can correct an off-center punch, insufficient support, weak profile, or incorrect punch-to-die relationship.
Diagnostizieren Sie Verschleiß und Bruch, bevor Sie den Stempel austauschen
The visible damage is not always the root cause. A symptom-based inspection reduces the risk of replacing the punch while leaving the system problem unchanged.
| Symptom | Mögliche Variablen | Erste Kontrollen |
| Die Mahlzeit nimmt allmählich zu | Kantenverschleiß, die wear, clearance change | Inspect punch edge, die opening, feature quality trend |
| Die Abnutzung tritt hauptsächlich auf einer Seite auf | Deflection, Fehlstellung, feed error, ungleichmäßiger Abstand | Check guides, pilots, holder position, die-button alignment |
| Kantenchips lokal | Shock, Übermäßige Last, Schlechte Unterstützung, low toughness, tight local clearance | Inspektion der Bruchstelle, punch support, die opening, Lastrichtung |
| Stempelbiegungen oder -schnallen | Übermäßige nicht unterstützte Länge, small section, Seitenlast, Überlastung | Check profile, Anleitung, station operation, strip position |
| Material haftet am Punch | Galling, Schlechte Schmierung, finish issue, ungeeignete Beschichtung | Inspect pickup pattern, stock surface, Schmierung, sidewall finish |
| Punch-Kopf versagt | Poor seating, weak backing support, Spannungskonzentration, Überlastung | Check holder, Rückplatte, head geometry, Kontaktmuster |
| Geschoss folgt dem Schlag | Haftung, vacuum effect, poor slug relief, Punch-Face-Bedingung | Inspect slug path, die relief, Punchface, Schmierung |
| Merkmale-Positionsdrifte | Feed, pilot, Leitfaden, Träger, or punch movement | Check strip pitch, pilot condition, Halterbefestigung, die alignment |
Repeated fracture deserves a broader investigation. The dedicated guide to Stanzbruch in Stempelwerkzeugen covers fracture causes and preventive actions in more depth.
A practical rule is to inspect the mating and supporting components whenever the same punch fails again. Replacing a damaged punch with an identical one will not correct a worn die button, loose holder, unstable feeder, damaged stripper, or misaligned guide system.
Plan Regrinding, Inspektion, and Interchangeable Replacement
Regrinding restores the cutting edge, but it also removes punch length. That change can affect penetration, stripper interaction, station timing, and the relationship with other punches.
A maintenance plan should define:
- the condition that triggers sharpening;
- allowable stock removal;
- original and remaining punch length;
- edge geometry after grinding;
- required straightness or runout;
- whether coating must be reapplied;
- inspection of the mating die button;
- timing or penetration adjustment after installation;
- the minimum remaining serviceable length.
Do not wait for severe chipping if the punch is intended to be reground. Grinding away extensive damage removes more material and may make it harder to preserve the original profile.
Replacement punches also need functional datums. A drawing should identify which surfaces control:
- position in the holder;
- working-tip location;
- head seating;
- overall operating length;
- profile orientation;
- relationship with the mating die opening.
SunshinePro states that its quality approach includes incoming inspection, In-Prozess-Überwachung, Endgültige Tests, und Inspektionsberichterstattung. For an actual order, the buyer should still define which dimensions, Datum, Toleranzen, and report fields must be verified.
Wählen Sie einen Standard- oder maßgefertigten Stempelstift
A standard punch may be suitable when the required profile, Abmessungen, Kopfstil, retention method, Material, and tolerances match an available design.
A custom punch is more likely to be required when the station uses:
- a non-round or proprietary profile;
- an unusual head or retention interface;
- a stepped or reduced working section;
- a special transition between shank and tip;
- an orientation feature;
- tight relationships between several datums;
- replacement dimensions tied to an existing die;
- a specific material, Wärmebehandlung, or coating combination.
| Auswahlfrage | Der Standard-Stempel könnte passen | Ein individueller Stanzer kann erforderlich sein |
| Is the working profile common? | Rundes oder etabliertes Katalogprofil | Special slot, contour, Schritt, or asymmetric shape |
| Is the holder interface standard? | Gemeinsamer Kopf- und Schaft-Konfiguration | Proprietäre Retention oder Sitzgeometrie |
| Are replacement datums simple? | Grundlegende Durchmesser- und Längenregelung | Multiple positional, Profil, or orientation controls |
| Is the material readily available in the required form? | Standard gelistete Steigung | Special grade, carbide form, or treatment requirement |
| Does the punch match an existing die? | Bereits verwendete Standardmaße | Exakte Austauschkompatibilität erforderlich |
A worn sample can help identify the component, but it may not preserve the original dimensions. Verschleiß, regrinding, Biegen, and edge damage can all distort the sample. A controlled drawing remains the preferred reference.
SunshinePro states that custom punch pins can be produced from drawings, Proben, or specifications, with custom dimensions, Formen, head profiles, Materialien, und Beschichtungen. Its published processes include CNC machining, Präzisionsschleifen, Wärmebehandlung, Vakuumwärmebehandlung, and EDM. Feasibility still needs to be confirmed for the specific geometry and tolerance combination.
Bereite die Zeichnung und das RFQ-Paket vor
A complete inquiry helps the supplier evaluate material, Herstellungsroute, Inspektion, and replacement requirements without guessing.
Einbeziehen:
- punch drawing and revision;
- station function: Piercing, Trimmen, Bildung, cutoff, or piloting;
- strip material grade;
- strip thickness;
- workpiece hardness or strength where relevant;
- stock coating or surface condition;
- working profile and feature dimensions;
- mating die-button dimensions or intended clearance;
- Shank, Kopf, Verbleib, and orientation details;
- functional datums;
- dimensional and geometric tolerances;
- required surface finish;
- Kantenbedingung;
- punch material and heat-treatment requirements;
- Beschichtungsanforderung, wenn bereits definiert;
- unsupported length and guidance arrangement;
- press speed or production rate;
- Erwartetes Produktionsvolumen;
- Schmierzustand;
- known failure symptoms;
- regrinding and spare-punch requirements;
- material certificate, Wärmebehandlungsbilanz, coating record, or inspection-report requirements.
Published tolerance or hardness ranges should not be copied into the RFQ without checking whether they suit the drawing. SunshinePro’s punch pages publish capability ranges up to ±0.002 mm and HRC 58–68, but the achievable combination depends on punch size, Profil, Material, Wärmebehandlung, Beschichtung, und Inspektionsmethode.
The most useful supplier question is not “How many cycles will this punch last?” without operating data. Ask the supplier to review the station conditions, identify manufacturing or inspection risks, and confirm the proposed material, Geometrie, and tolerance approach.
For a drawing-based feasibility review or quotation, submit the punch specification, strip information, station function, and known failure history through the SunshinePro-Kontaktseite.
Teilen:



Geschrieben von Sunshine
Bei Sunshine, Wir sind ein professioneller Hersteller und Lieferant von Präzisionsformkomponenten, bietet ein breites Produktsortiment für Stange- und Spritzgussanwendungen. Unser Kernfokus liegt auf dem Stanzen von Stempeln, Auswurfstifte und -hülsen, sowie Führungspfosten und Buchsen. Mit fortschrittlicher CNC-Bearbeitung, Strenge Qualitätskontrolle, und starke Produktionskapazitäten, Wir sorgen für Zuverlässigkeit, Hochpräzisionsteile, zusammen mit vorrätigen Standardkomponenten für schnelle und effiziente weltweite Versorgung.
NACHRICHTEN
EMPFANG SERVICE
Mit hochwertigen Teilen für jedes Budget und freundlichem Personal, das geschult ist, um Ihren Besuch informativ und unkompliziert zu gestalten.
