



Kriterien zur Überholung von Tablet-Werkzeugen: Reparatur, Neuanstrich, oder ersetzen
Tablet tooling refurbishment criteria should separate three very different conditions. Minor surface damage may be repairable. A worn functional coating may justify recoating when the underlying tool remains sound. Risse, lost geometry, deep pitting, or dimensions outside approved limits usually point toward replacement.
The decision applies to tablet compression punches and dies, not to electronic-tablet tools. Readers who need broader context on tooling configurations can first review Typen der Tabletpress-Werkzeuge. This guide stays focused on the condition assessment that determines whether existing tooling can return to service.
No single public wear limit applies to every punch or die. The final acceptance basis should come from the approved drawing, tooling specification, internal SOP, validated process requirements, and the measured history of the tooling set.
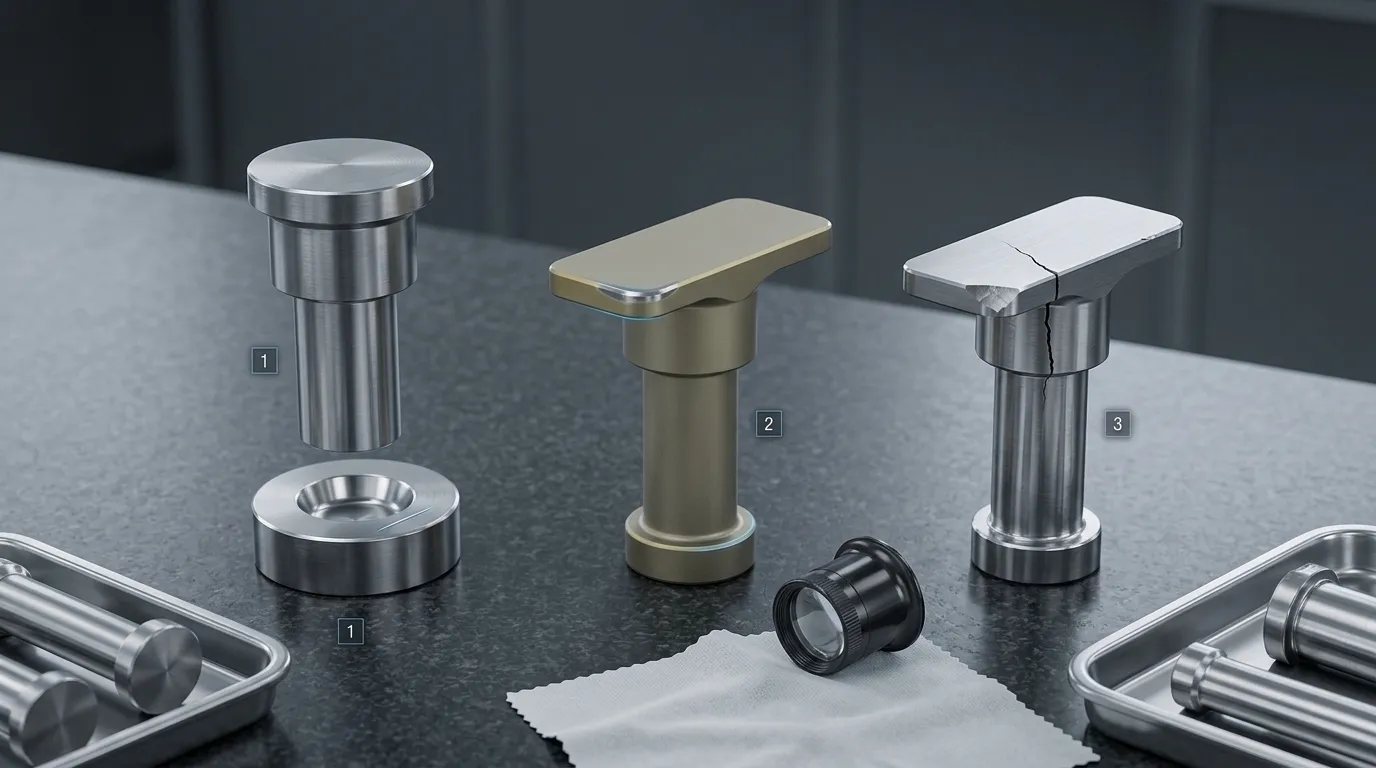
Reparatur, Neuanstrich, oder ersetzen: The Decision at a Glance
A visible defect does not automatically determine the correct action. The location, Tiefe, remaining geometry, Substratzustand, coating history, and effect on the complete tooling set all matter.
| Beobachteter Zustand | Wahrscheinliche Anlage | Erforderliche Überprüfung | Grund |
|---|---|---|---|
| Light burr, shallow scratch, small nick, early J-hook, or limited surface corrosion | Eine kontrollierte Reparatur ist möglicherweise möglich | Vergrößerte Inspektion und Maßprüfungen vor und nach der Materialentfernung | Kleinere Oberflächenschäden können entfernt werden, ohne kritische Geometrie zu verlieren |
| Worn, beschädigt, or partially detached coating with sound base material | Eine Neubeschichtung kann in Betracht gezogen werden | Coating removal assessment, substrate inspection, dimensional verification, and post-coating inspection | Der Fehler kann auf die funktionale Oberfläche beschränkt sein |
| Lost land, altered cup profile, excessive working-length variation, or die-bore wear outside approved limits | Ersetzen oder eine fachärztliche Überprüfung einholen | Comparison with the approved drawing, specification, and set measurements | Beschichtung oder Polieren kann fehlende Geometrie nicht wiederherstellen |
| Crack, severe chip, deep pitting, Verformung, or uncertain structural integrity | Ersetzen | Dokumentierte Ablehnung und Überprüfung der Ursache | Continued use may increase breakage, Kontamination, and tablet-quality risks |
| Der Zustand kann nicht zuverlässig gemessen oder nachverfolgt werden | Halten Sie für eine fachärztliche Überprüfung oder Austausch | Confirm tool identity, drawing revision, Material, Beschichtung, and maintenance history | Ein Werkzeug sollte nicht in die Produktion zurückkehren, wenn Konformität nicht nachgewiesen werden kann |
“Specialist review” is a valid disposition. Maintenance teams should not force an uncertain tool into a repair or replacement category before the necessary measurements and material assessment are available.
Stellen Sie die Beweise fest, bevor Sie eine Entscheidung treffen
The condition of a punch or die should be documented before polishing, Bearbeitung, coating removal, or any other operation changes the evidence.
A controlled assessment normally follows this sequence:
- Segregate and identify the tooling. Record the tool number, set, Position, Material, Beschichtung, drawing revision, and production batch or campaign where the issue appeared.
- Clean and dry the components. Residue can hide corrosion, Punktewertung, coating failure, and fine cracks.
- Review the service history. Check previous polishing, Reparaturen, working-length corrections, coating cycles, and recurring defects.
- Conduct visual and magnified inspection. Examine tablet-forming surfaces, contact surfaces, guidance areas, Schlüssel, edges, und Stanzrohre.
- Measure critical dimensions. Use calibrated instruments and an approved inspection method.
- Compare each component with the specification and the set. A tool can pass an isolated dimensional check but still create inconsistency if it no longer matches the rest of the set.
- Assign a provisional disposition. Reparatur, recoat, specialist review, or replace.
- Record the original condition. Photographs and before-service measurements help establish what work was performed and how much material was removed.
In regulated drug manufacturing, equipment cleaning and maintenance should follow written procedures under 21 CFR 211,67. Measuring devices should also be controlled under an appropriate calibration program, as addressed by 21 CFR 211.160. These requirements do not provide punch or die wear limits, but they support controlled inspection, documented responsibilities, and reliable measurements.
Treat Tablet Defects as Inspection Triggers, Not Proof
Sticking, Picking, Begrenzung, Laminierung, Blitz, difficult ejection, or inconsistent tablet dimensions can justify a tooling inspection. They do not prove that worn tooling is the sole cause.
Tablet defects may also involve:
- Formulierungseigenschaften;
- granulation condition;
- lubricant distribution;
- tablet shape and embossing;
- compression force;
- Presseaufbau;
- Zubringerleistung;
- Verweilzeit;
- environmental conditions.
Research on punch-surface evolution shows that sticking behaviour can depend on the powder, Kompressionsbedingungen, Laufzeit, and punch-surface quality rather than one isolated factor. The study is indexed in PubMed. A broader technical review of tablet scoring and manufacturing defects also describes the interaction among formulation, Konstruktion, Werkzeuge, and process variables in Angewandte Wissenschaften.
Production symptoms should guide the inspection location. They should not replace dimensional measurement or root-cause analysis.
Use the Correct Drawing, Spezifikation, and Tool History
Die korrekten Referenzdokumente müssen identifiziert werden, bevor jemand entscheidet, dass ein Werkzeug "innerhalb der Toleranz" liegt.
The assessment record should confirm:
- tooling format and component type;
- unique tool or set identification;
- approved drawing and revision;
- specified material;
- coating type and history, Wo zutreffend;
- required critical dimensions;
- internal acceptance limits;
- previous repair or rework;
- previous coating removal and recoating;
- recorded production or maintenance problems.
Generic internet values should not replace approved limits. Even tools that appear similar may have different cup geometry, Landbreite, Arbeitsdauer, Kopfkonfiguration, Beschichtung, oder Anwendungsanforderungen.
The service history is particularly important because every polishing or machining operation may remove material. A component that tolerated one minor repair may have less restoration margin after several earlier interventions.
Wenn eine kontrollierte Reparatur angemessen sein kann
Controlled repair is most appropriate when damage is limited, Barrierefrei, and removable without taking the component outside its approved geometry.
Potentially repairable conditions may include:
- small burrs;
- shallow scratches;
- minor nicks;
- light surface corrosion;
- early J-hook formation;
- slight surface deterioration;
- localized roughness that has not penetrated deeply into the substrate.
These descriptions are not automatic approval criteria. A shallow scratch on a non-critical area may be less serious than a similar mark across the punch cup, Land, key, or die bore.
The technician must consider:
- defect depth;
- defect location;
- amount of material that must be removed;
- remaining land or edge geometry;
- Pokalprofil;
- Arbeitsdauer;
- coating status;
- effect on the tooling set.
Controlled polishing can remove minor imperfections, but it also removes tool material. Technische Anleitung von Pharmazeutische Technologie recommends inspection, repair, measurement, and polishing as separate stages rather than treating polishing as the entire maintenance process. Natolis Anleitung zur Haltung von Stempeln also warns that unnecessary refurbishment removes material and that not every wear condition is repairable.
The goal is not to make a component look new. The goal is to remove the defect while preserving approved geometry and function.
Was nach der Entfernung des Materials überprüft werden muss
Any repair that removes material should be followed by another inspection.
Depending on the affected component, this may include:
- punch working length;
- cup depth and profile;
- embossing condition;
- land width and continuity;
- punch-tip shape;
- head-flat condition;
- head angle;
- barrel condition;
- key or orientation feature;
- die-bore dimensions;
- consistency with the rest of the set.
Before-and-after measurements should be retained in the tooling history. A visually smooth surface is not enough if the repair has altered the cup, shortened the punch, reduced the land excessively, or created variation across the set.
Das Wiederbeschichten ist technisch vertretbar
Recoating should be considered only when the functional coating is the main failure and the underlying tool remains suitable for service.
Possible coating-related evidence includes:
- localized wear-through;
- coating delamination;
- reduced surface performance;
- freiliegendes Substrat;
- coating damage from handling or service;
- deterioration that contributes to friction or product adhesion.
Before recoating, the assessment should answer five questions.
- Can the existing coating be removed without damaging the tool?
The stripping process must be compatible with the substrate, Geometrie, and existing surface condition. - Is the substrate structurally sound?
The tool should be checked for cracks, severe corrosion, deep pitting, Verformung, and hidden damage beneath the coating. - Do the critical dimensions still conform?
Coating renewal should not be used to disguise lost land, veränderte Bechergeometrie, excessive working-length variation, or die-bore wear. - Is the replacement coating compatible with the application?
Material, Formulierungsverhalten, operating conditions, and the original tooling specification may affect the choice. - Can the finished tool be verified after recoating?
Oberflächenzustand, coating coverage, affected dimensions, and set consistency should be inspected before release.
A refurbishment supplier may use coating removal, Oberflächenvorbereitung, and coating application as separate controlled stages. The exact process and acceptance method should be confirmed with that supplier. SunshinePro’s published website does not verify that it offers coating stripping or recoating, so those services should not be assumed.
Was eine Neubeschichtung nicht beheben kann
Recoating changes the functional surface. It does not rebuild missing base material.
It cannot correct:
- a cracked punch or die;
- a severely chipped edge;
- deep substrate pitting;
- lost cup geometry;
- an excessively reduced land;
- unacceptable working-length variation;
- a deformed head or barrel;
- a damaged key;
- die-bore geometry outside approved limits;
- uncertain substrate integrity.
A new coating over a nonconforming substrate may improve appearance while leaving the underlying failure unresolved.
Bedingungen, die auf einen Ersatz hindeuten
Replacement becomes the stronger technical choice when a component cannot be restored and verified without compromising its function or safety.
Common replacement indicators include:
- visible or suspected cracking;
- severe chipping;
- missing material;
- deep corrosion or pitting;
- Verformung;
- unacceptable working length;
- irrecoverable cup or embossing geometry;
- excessive land loss;
- severely worn head or barrel features;
- damaged orientation keys;
- die-bore wear outside approved limits;
- recurring failure after previous repair or recoating;
- unknown material or coating history;
- inability to identify the correct drawing or acceptance specification.
The seriousness of a defect also depends on its position. Damage on a tablet-forming surface may affect tablet appearance, Veröffentlichung, or dimensional consistency. Damage on a punch head, Lauf, or key may affect movement, Ausrichtung, or interaction with the press. Die-bore damage can influence compression, Auswurf, Blitz, und Tablet-Integrität.
Technical suitability should be decided before cost. A low repair quotation does not make a structurally damaged or dimensionally nonconforming tool acceptable.
Betrachten Sie das gesamte Werkzeugset und seine Überholungsgeschichte
A punch or die should not always be judged in isolation.
One repaired punch may create set-level variation if its:
- working length differs from the others;
- cup depth has changed;
- land has been altered;
- head geometry no longer matches;
- coating thickness or surface condition differs;
- prior repair history is substantially different.
The complete tooling record should show how many times each component has been polished, machined, corrected, or recoated. There is no universal safe maximum number of refurbishments. One light repair may remove less material than another aggressive intervention.
Recurring damage may also indicate a wider unresolved issue, such as press alignment, Handhabung, Reinigung, storage, formulation abrasiveness, corrosive exposure, or excessive operating load. Replacing the tool without investigating the cause may only restart the same failure cycle.
Bewerten Sie Schläge und Sterben nach ihren kritischen Eigenschaften
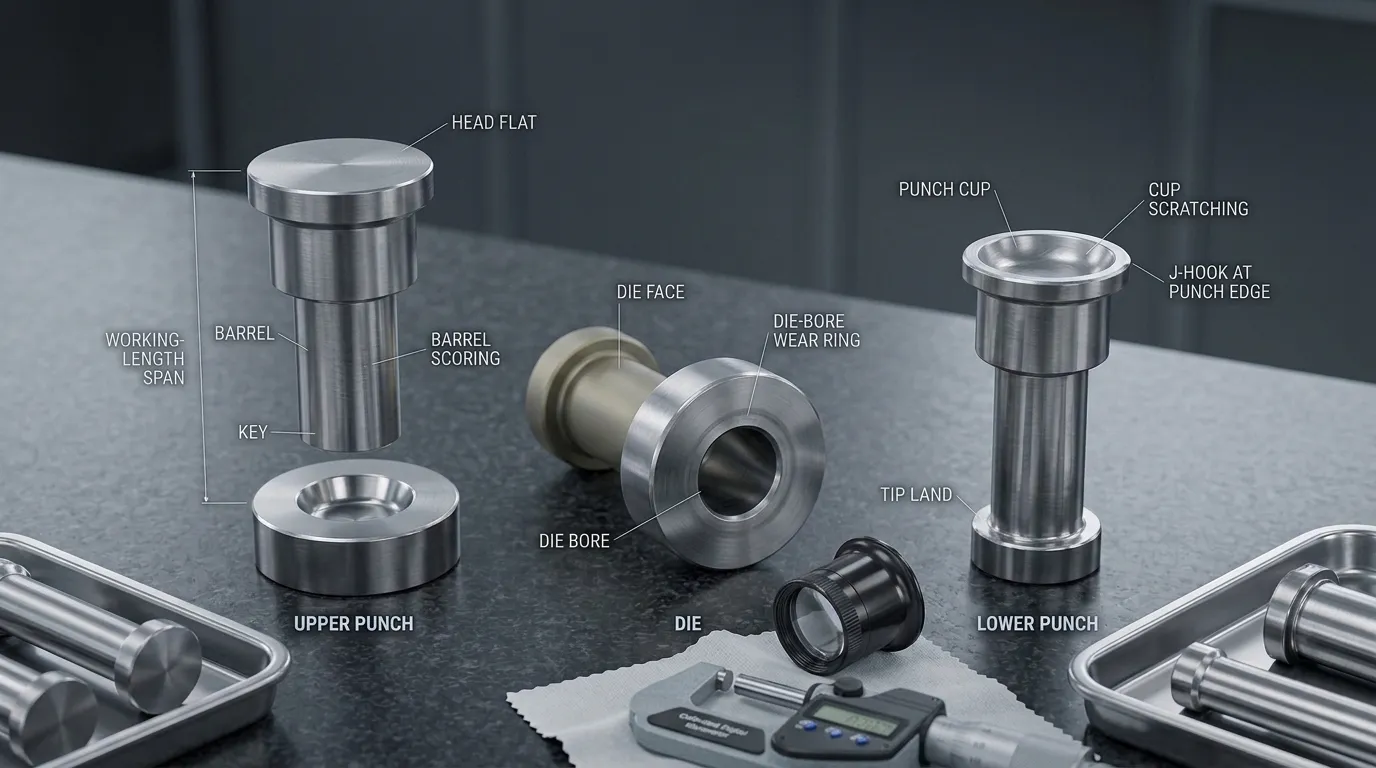
Different tooling features perform different functions. The inspection should therefore connect each defect to the feature it affects.
| Ausstattung | Bedingungen zu überprüfen | Warum es wichtig ist |
| Punschbecher und Prägung | Kratzer, Gruben, coating loss, profile damage, filled or rounded detail | Diese Oberflächen bilden das Tablet-Gesicht und die Markierungen |
| Punch-Tip-Land | Mahlscheiben, J-hook, uneven width, Chipping, material loss | Land condition can affect tablet edges, Veröffentlichung, and structural behaviour |
| Arbeitslänge | Abweichung von genehmigten Grenzen oder dem Werkzeugsatz | Arbeitslängeninkonsistenz kann die Kompression und die Konsistenz der Tabletten beeinflussen |
| Schlagkopf und flacher Kopf | Verschleiß, Verformung, Punktewertung, altered contact surface | Diese Bereiche interagieren mit den Presskomponenten und beeinflussen die Kraftübertragung |
| Lochlauf | Punktewertung, Korrosion, excessive wear, Verformung | Der Zustand des Laufs beeinflusst Führung und Bewegung |
| Schlüssel- oder Orientierungsmerkmal | Verschleiß, Lockerheit, Schäden, incorrect position | Orientierungsmerkmale steuern die Ausrichtung der Stanz |
| Die face | Handling damage, Korrosion, Chips, Mahlscheiben | Gesichtsschäden können die Installation und Ausrichtung beeinflussen |
| Die bore | Ring tragen, Punktewertung, Korrosion, Taper, surface deterioration | Bore condition affects tablet formation, Kompression, und Auswurf |
Punch-Funktionen zur Überprüfung
The punch cup, Prägung, Land, Arbeitsdauer, Kopf, Lauf, and key should be assessed separately.
A small surface mark in the cup may be repairable if it can be removed without changing the profile. A chipped embossing feature or deeply pitted cup may require replacement because the tablet-forming geometry cannot be recreated reliably through polishing.
Early J-hook development at the punch edge may sometimes be corrected through controlled restoration. Severe edge loss is different. Removing enough material to eliminate it may reduce the land or alter the tablet profile.
Head and barrel defects should not be ignored simply because they do not contact the tablet. These features control how the punch moves and interacts with the press. Punktewertung, Verformung, or wear can affect alignment and loading.
Würfel-Features zur Bewertung
The die bore should be checked for:
- wear rings;
- Punktewertung;
- Korrosion;
- Gruben;
- taper or dimensional change;
- Rauheit;
- localized coating failure;
- damage near the entry or compression zone.
Die-bore wear may contribute to poor ejection, Begrenzung, Blitz, und dimensionale Inkonsistenz, but measurement is required before assigning the cause. The detailed metrology process belongs in a dedicated guide to Messung des Tablettmatrizenbohrungsverschleißes.
The die face and external installation surfaces should also be inspected for burrs, handling damage, and deformation that may affect seating or alignment.
Überprüfe generalüberholte Werkzeuge, bevor sie wieder in Produktion gehen.
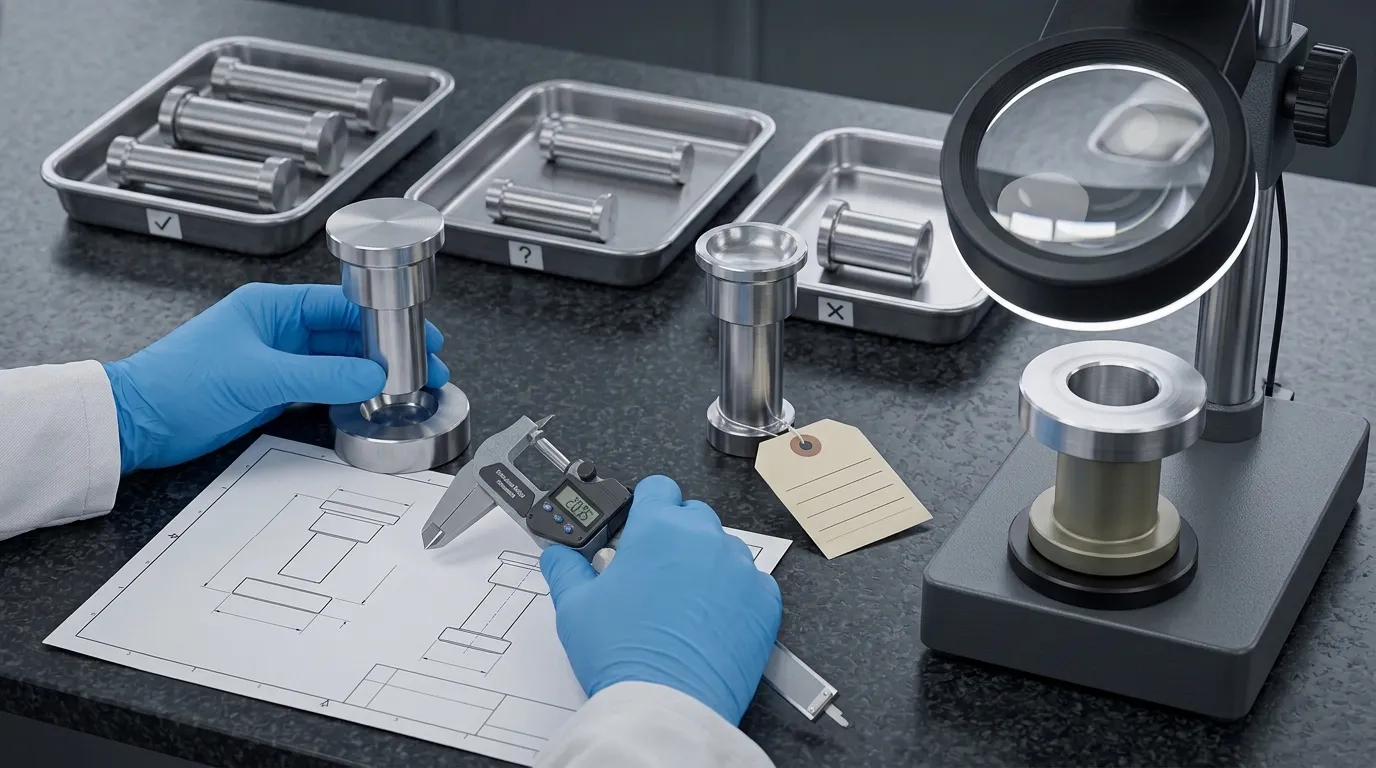
A completed repair or coating operation is not the same as release approval. The affected tool should be inspected again after the work is finished.
A practical release checklist includes:
- repeat visual and magnified inspection;
- verify that the original defect has been removed or controlled;
- measure all affected critical dimensions;
- compare the component with the approved specification;
- compare the component with the rest of the tooling set;
- inspect repaired edges, Ländereien, Becher, Kopf, Läufe, Schlüssel, and die bores as applicable;
- confirm coating coverage and surface condition where recoating was performed;
- verify cleanliness and corrosion protection;
- record the work completed;
- record before-and-after dimensions;
- identify the technician and approver;
- document the final disposition.
For regulated pharmaceutical operations, 21 CFR 211.182 addresses chronological equipment cleaning and maintenance records. Die EU GMP Band 4 Rahmen also supports controlled equipment, Dokumentation, Produktion, and quality-system practices.
These sources establish the need for controlled procedures and records. They do not establish a universal acceptable scratch depth, Landbreite, Arbeitsdauer, or die-bore limit. Those limits must come from the applicable technical documentation and approved quality system.
Bewerten Sie einen Überhol- oder Ersatzanbieter
A supplier should be able to explain not only what work it can perform, but how it determines that the finished tooling remains fit for service.
Before sending tooling for refurbishment, Fragen Sie:
- How is the initial condition documented?
- Which dimensions are measured before work begins?
- Which defects are accepted for repair?
- Which defects trigger rejection?
- How much material may be removed?
- Can the existing coating be identified and removed safely?
- How is the substrate inspected after coating removal?
- Which dimensions are rechecked after repair or recoating?
- How is tooling-set consistency evaluated?
- What records accompany the completed tooling?
- What happens if the component fails final inspection?
- How are individual tools identified and traced?
- Can the supplier produce replacement tooling from the approved drawing or sample?
Do not assume that a new-tool manufacturer also provides used-tool repair or recoating. Those capabilities require separate confirmation.
When replacement is the technically correct decision, SunshinePro präsentiert Tabletpress-Werkzeuge for punches and dies, including standard and non-standard sizes and custom processing from drawings or samples. Its product page also lists high-speed steel, CNC-Bearbeitung, Wärmebehandlung, material inspection reports, and an inspection-and-delivery workflow for new tooling.
Provide the approved drawing, Beispiel, tooling format, material requirement, and inspection expectations when requesting a capability review. For a replacement-tooling discussion, use SunshinePro’s Kontaktseite rather than assuming that a damaged component can be refurbished.
Teilen:



Geschrieben von Sunshine
Bei Sunshine, Wir sind ein professioneller Hersteller und Lieferant von Präzisionsformkomponenten, bietet ein breites Produktsortiment für Stange- und Spritzgussanwendungen. Unser Kernfokus liegt auf dem Stanzen von Stempeln, Auswurfstifte und -hülsen, sowie Führungspfosten und Buchsen. Mit fortschrittlicher CNC-Bearbeitung, Strenge Qualitätskontrolle, und starke Produktionskapazitäten, Wir sorgen für Zuverlässigkeit, Hochpräzisionsteile, zusammen mit vorrätigen Standardkomponenten für schnelle und effiziente weltweite Versorgung.
NACHRICHTEN
EMPFANG SERVICE
Mit hochwertigen Teilen für jedes Budget und freundlichem Personal, das geschult ist, um Ihren Besuch informativ und unkompliziert zu gestalten.
